Target Reaction
OER duty, desired process result, competing reactions and product-quality responsibility.
Iridium MMO Anode Manufacturer · Oxygen-Evolution Duty
Custom IrO₂-rich and Ir-Ta MMO titanium anodes reviewed against the target anodic reaction, complete electrolyte, contaminants, electrical loading, effective coated area, cell geometry, connection and design-life basis.
Selection boundary: IrO₂-rich and Ir-Ta are related OER coating directions, not interchangeable product labels. Final selection requires the reaction, bath chemistry, contaminants, temperature, electrical duty, active-area convention and qualification method.
Start by confirming oxygen evolution and the complete operating window. Do not select an iridium coating from the application name or a single pH/current value.
OER duty, desired process result, competing reactions and product-quality responsibility.
Full composition, acidity, chloride, fluoride, additives, metals, contaminants and cleaning media.
Total current, voltage/reference basis, density denominator, duty, peaks and polarity.
Active area, gap, flow, connection, temperature, schedule, life method and end point.
Application names are routing labels. Each project still needs bath chemistry, target anodic reaction, current basis, temperature and acceptance evidence.
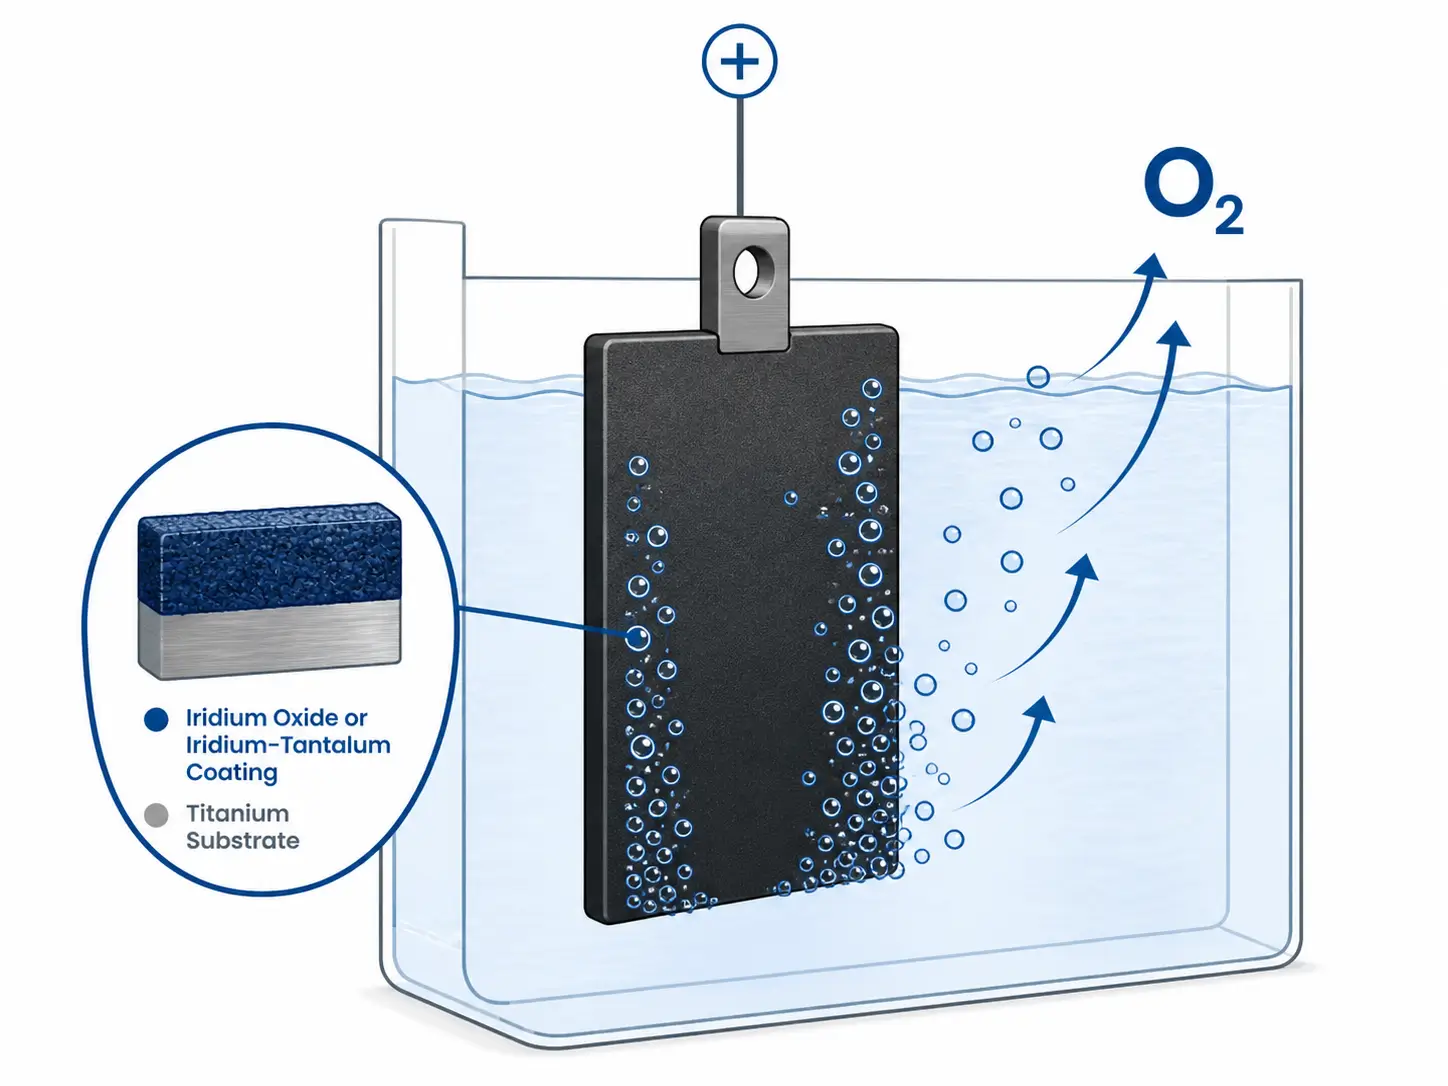
Confirm the intended OER duty, complete electrolyte, acidity, chloride/fluoride and other contaminants, temperature, flow, current-density basis and gas management.
Define bath chemistry, metal/additives, target anodic reaction, product-quality requirement, current distribution, temperature, cleaning and maintenance.
Provide metal-ion system, acidity, impurities, OER/side reactions, current duty, spacing, flow, deposit/product targets and process ownership.
Use only after environment, reaction/protection duty, output, connection, installation, monitoring and applicable project basis are confirmed.
Do not treat one bath result as proof for every chromium process. Confirm the chromium bath, additives, target reaction, temperature, current distribution, product-quality requirement, cleaning and supplier-approved operating window.
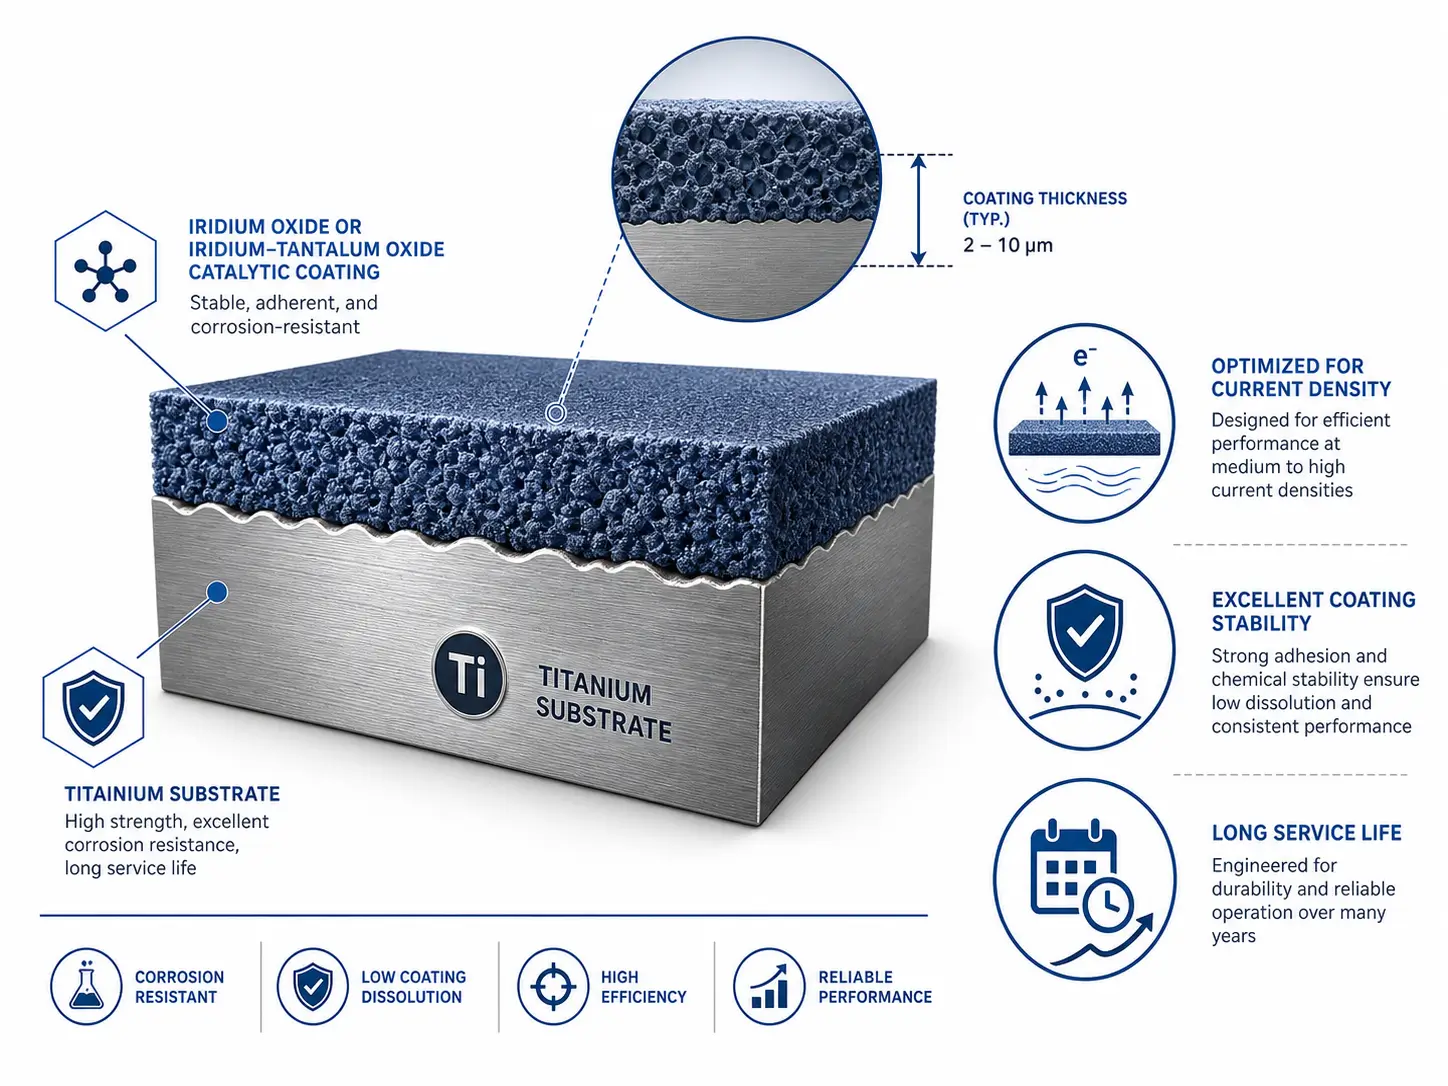
The coating family is selected against the actual OER process. Composition, loading, thickness and performance metrics require separate definitions and methods.
| Coating direction | Engineering role | Required inputs |
|---|---|---|
| IrO₂-rich MMO | OER duty under a process-specific electrolyte and electrical basis | Reaction, electrolyte, pH/acidity, contaminants, current density, temperature |
| Ir-Ta mixed oxide | OER service requiring a defined balance of coating and operating requirements | Complete chemistry, duty, potential/current basis, temperature, qualification |
| Project-specific iridium MMO | Existing specification, replacement or special process review | Controlled coating basis, active area, service history, failure evidence, validation |
The table defines what must be agreed. It does not publish universal current density, pH, temperature, fluoride, loading or life limits.
| Characteristic | RFQ / PO definition | Evidence when ordered |
|---|---|---|
| Titanium substrate | Grade/UNS, product-form standard, condition, geometry, tolerances and lot identity | MTC and traceability |
| Iridium MMO coating | IrO₂-rich / Ir-Ta / controlled performance basis, metric, units and active zones | Batch/process records and agreed coating evidence |
| Electrical duty | Current, voltage/reference, density denominator, duty, peaks, polarity and distribution | Project-specific electrical/electrochemical evidence |
| Geometry & connection | Dimensions, coated/masked zones, welds, tab/cable/feed, seal and mounting | Drawing and inspection report |
| Design life | Chemistry, temperature, current duty, cleaning, end point, method and exclusions | Calculation, qualification or agreed ALT record |
Geometry is selected with electrolyte access, gas release, active-area basis, current distribution, equipment layout, supports and electrical connection.
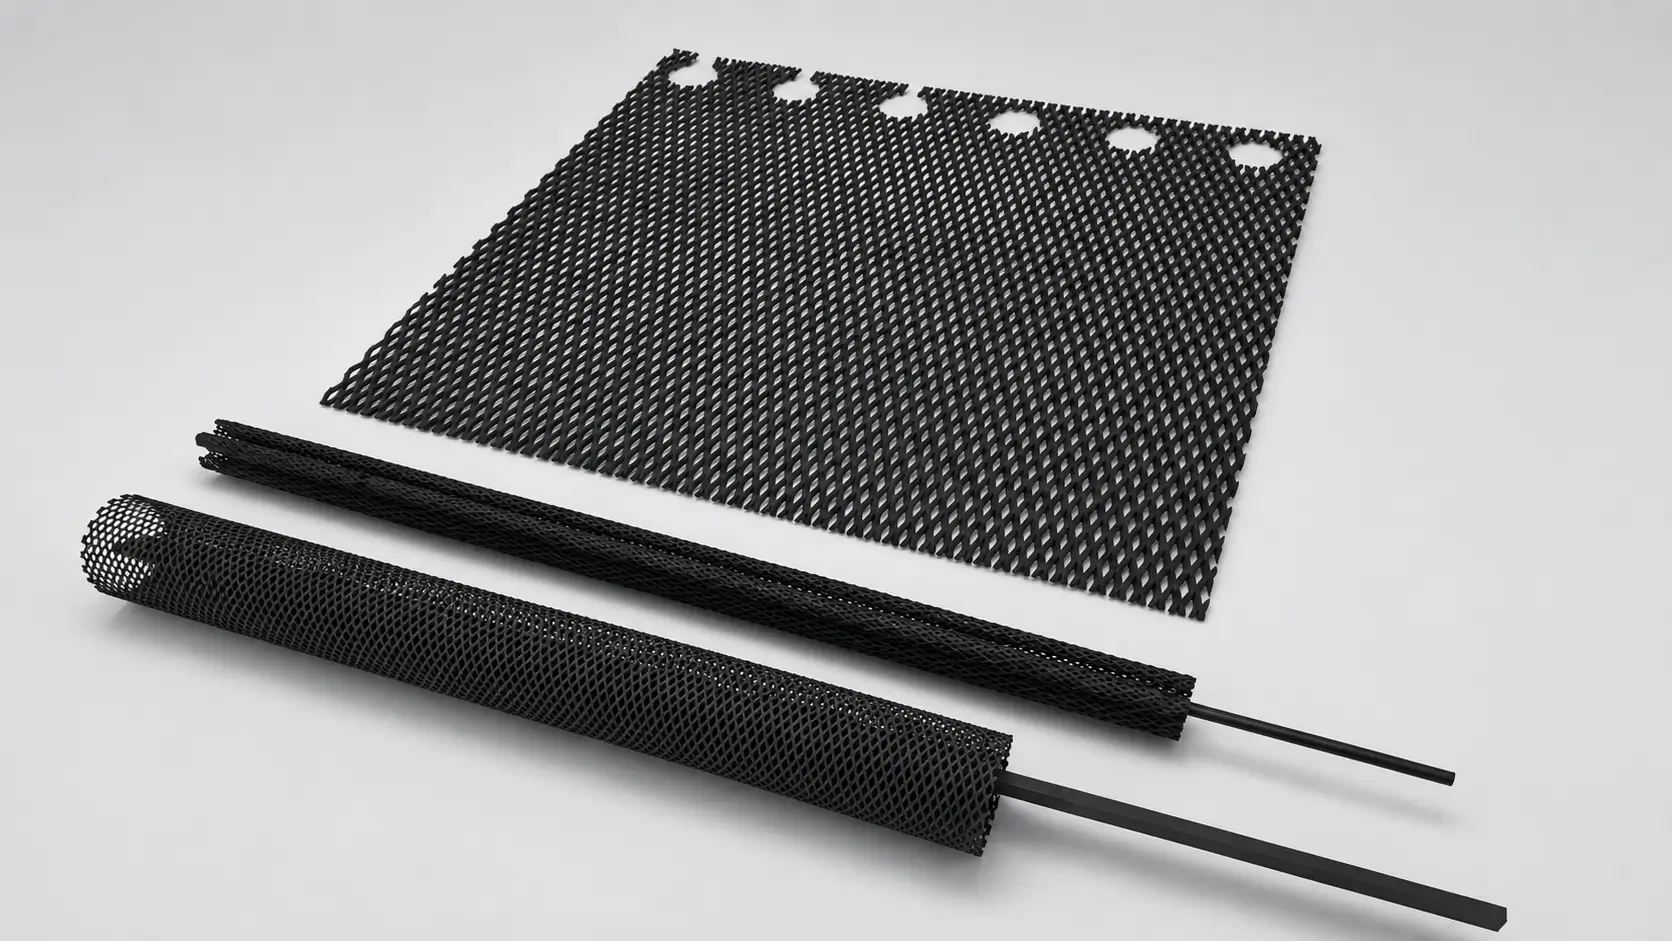
Open geometry for electrolyte access and distributed coated area. Define opening/strand, area convention, coated sides, frame and feed.
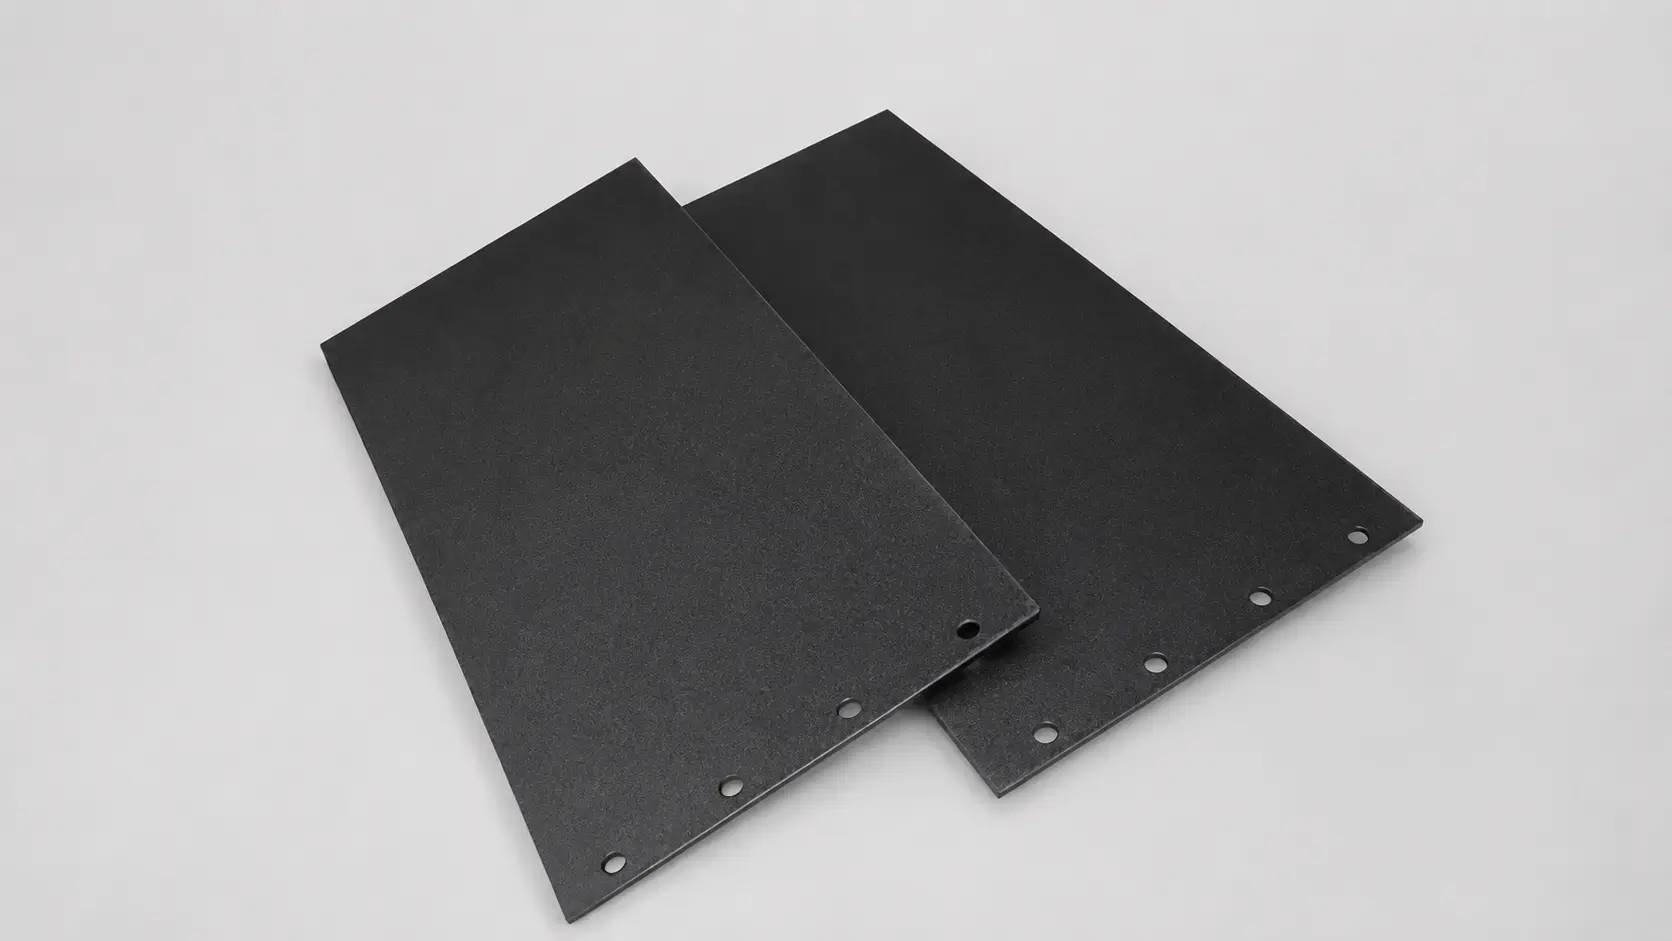
Flat or formed surfaces with controlled thickness, active faces, masking, tabs, mounting and electrode spacing.
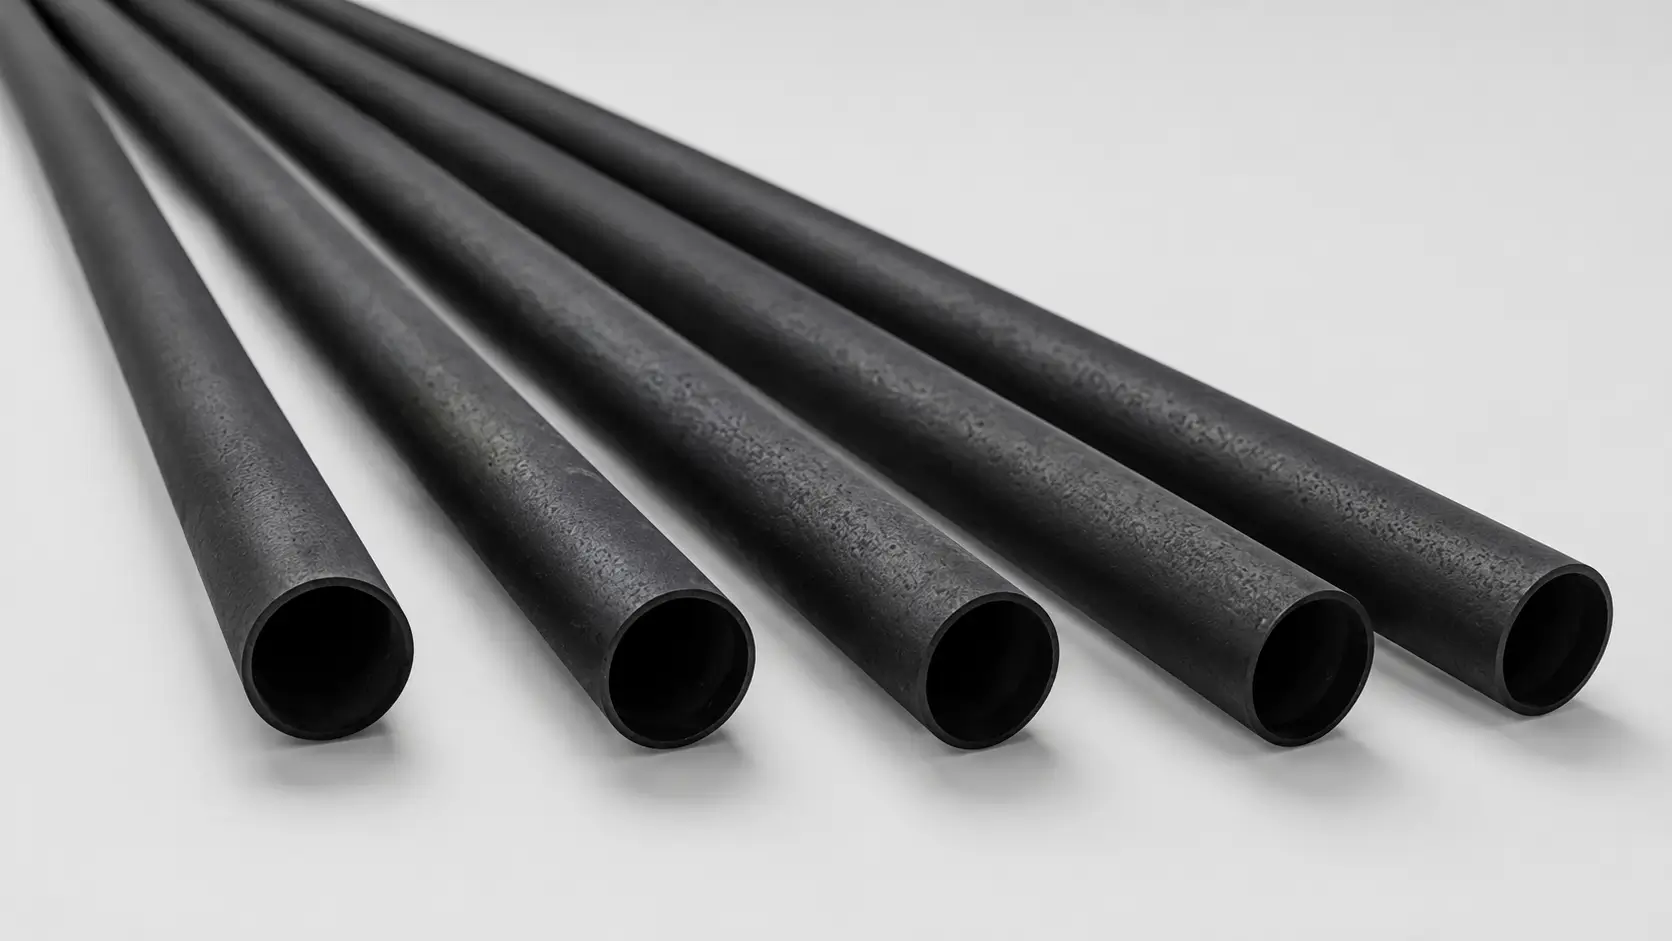
Cylindrical geometry defined by OD, wall where applicable, active length, ends, connection and installation.
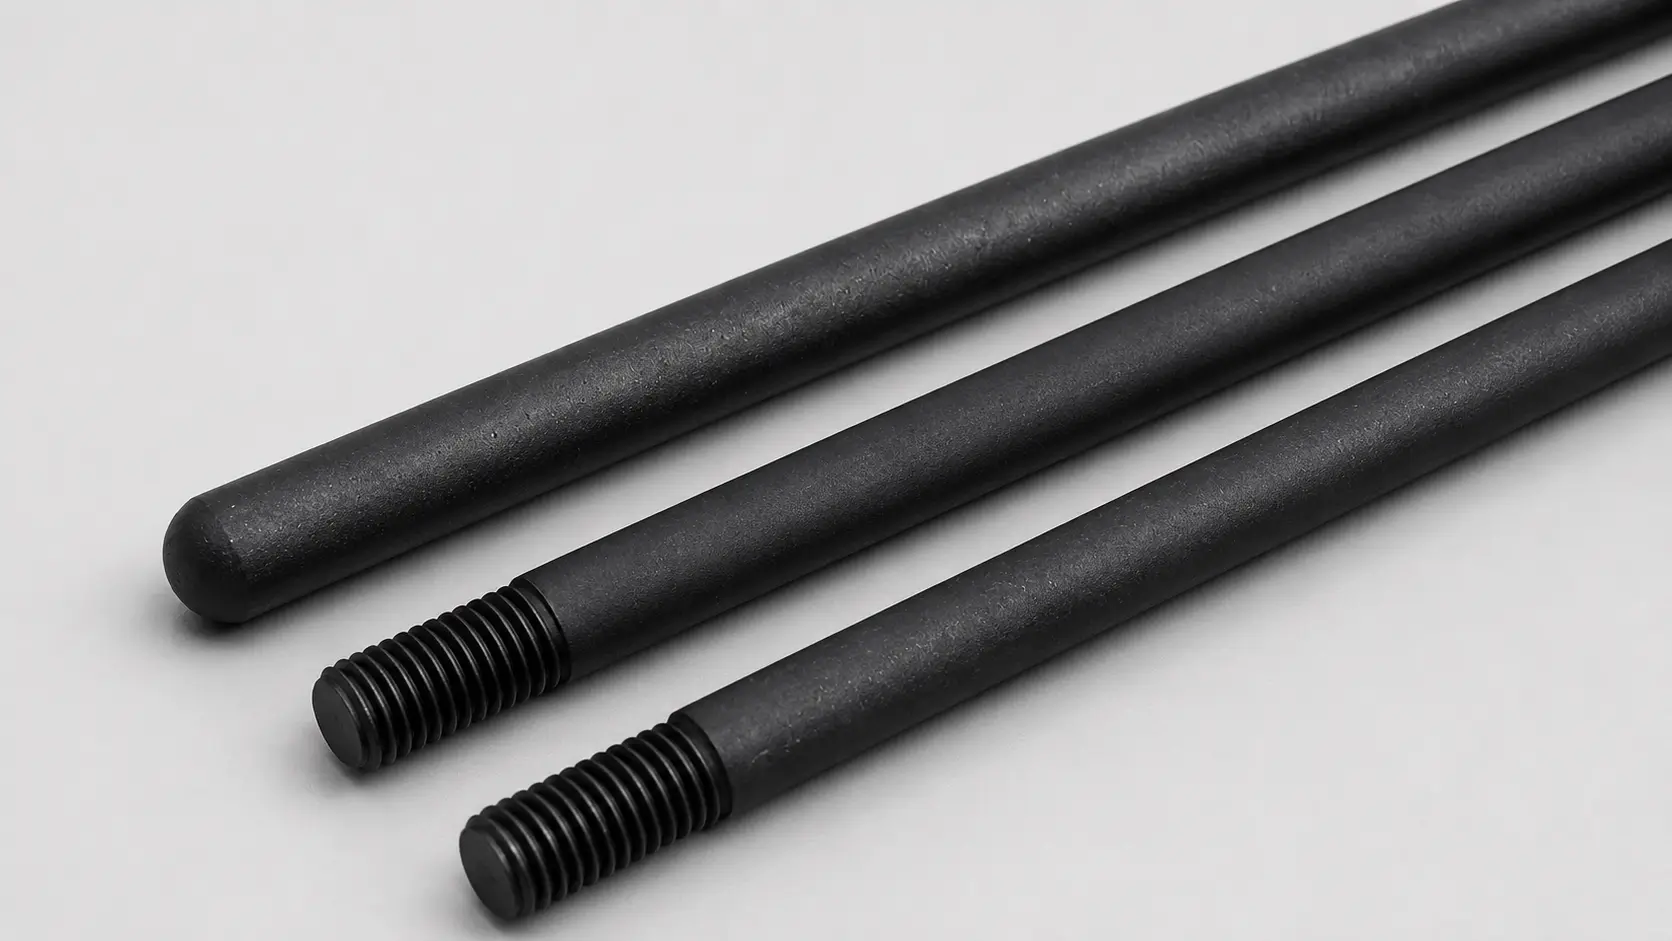
Compact electrodes defined by diameter, insertion/active length, thread or tab, mounting and current path.
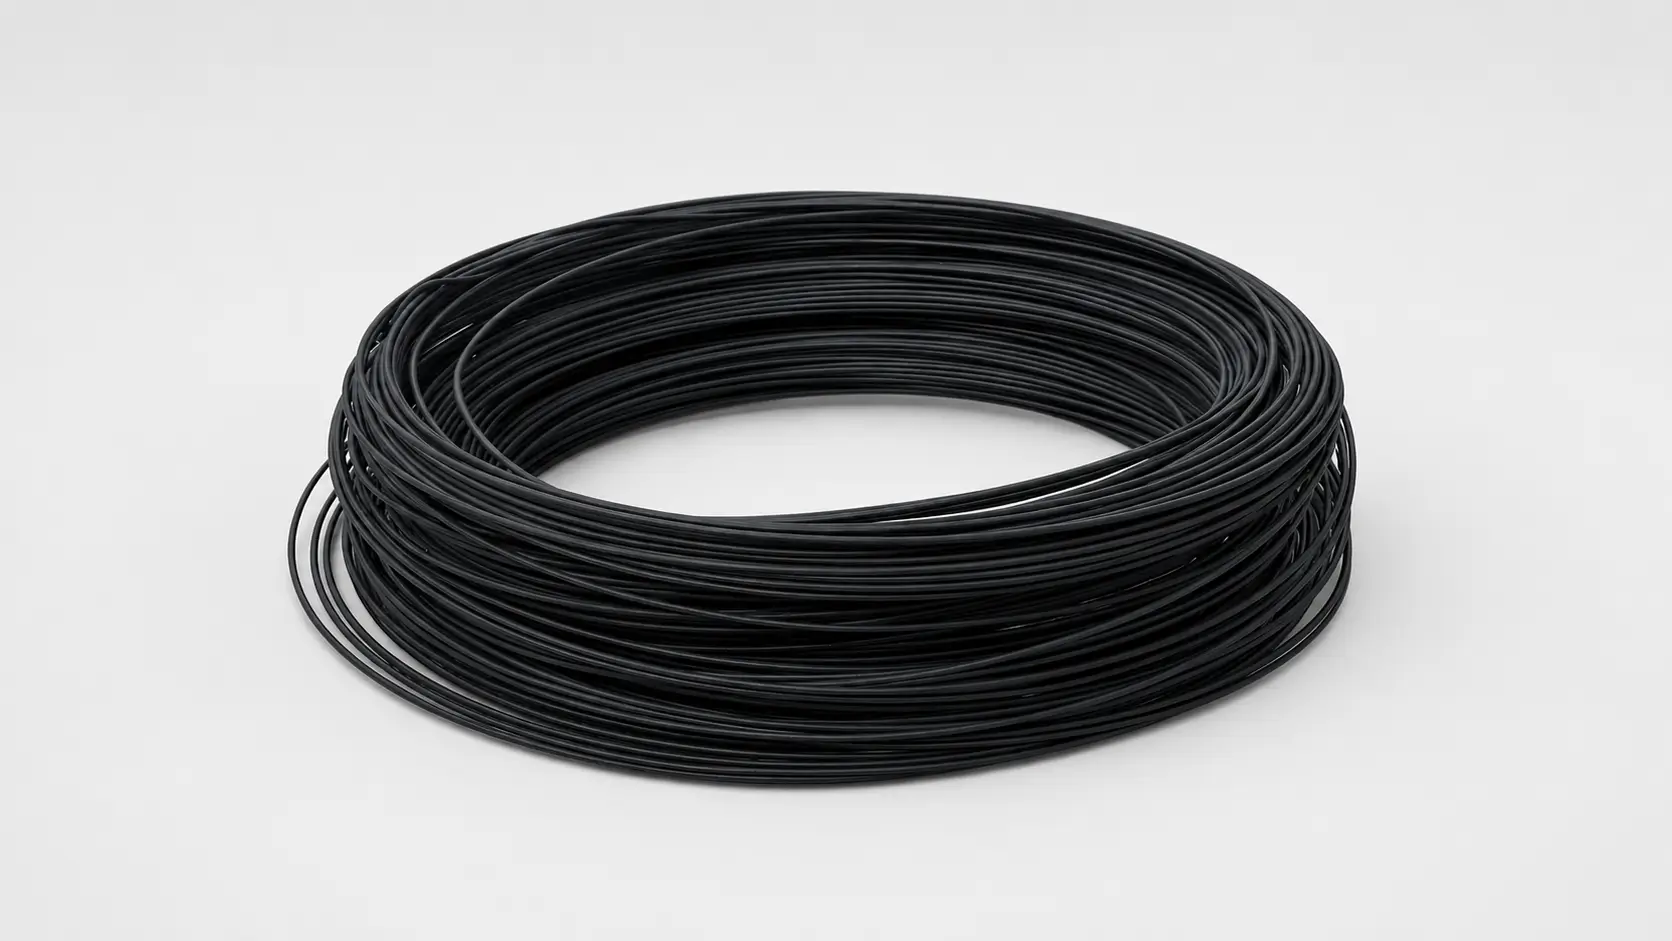
Wire or formed-wire electrodes controlled by diameter, active zone, routing, supports and termination.
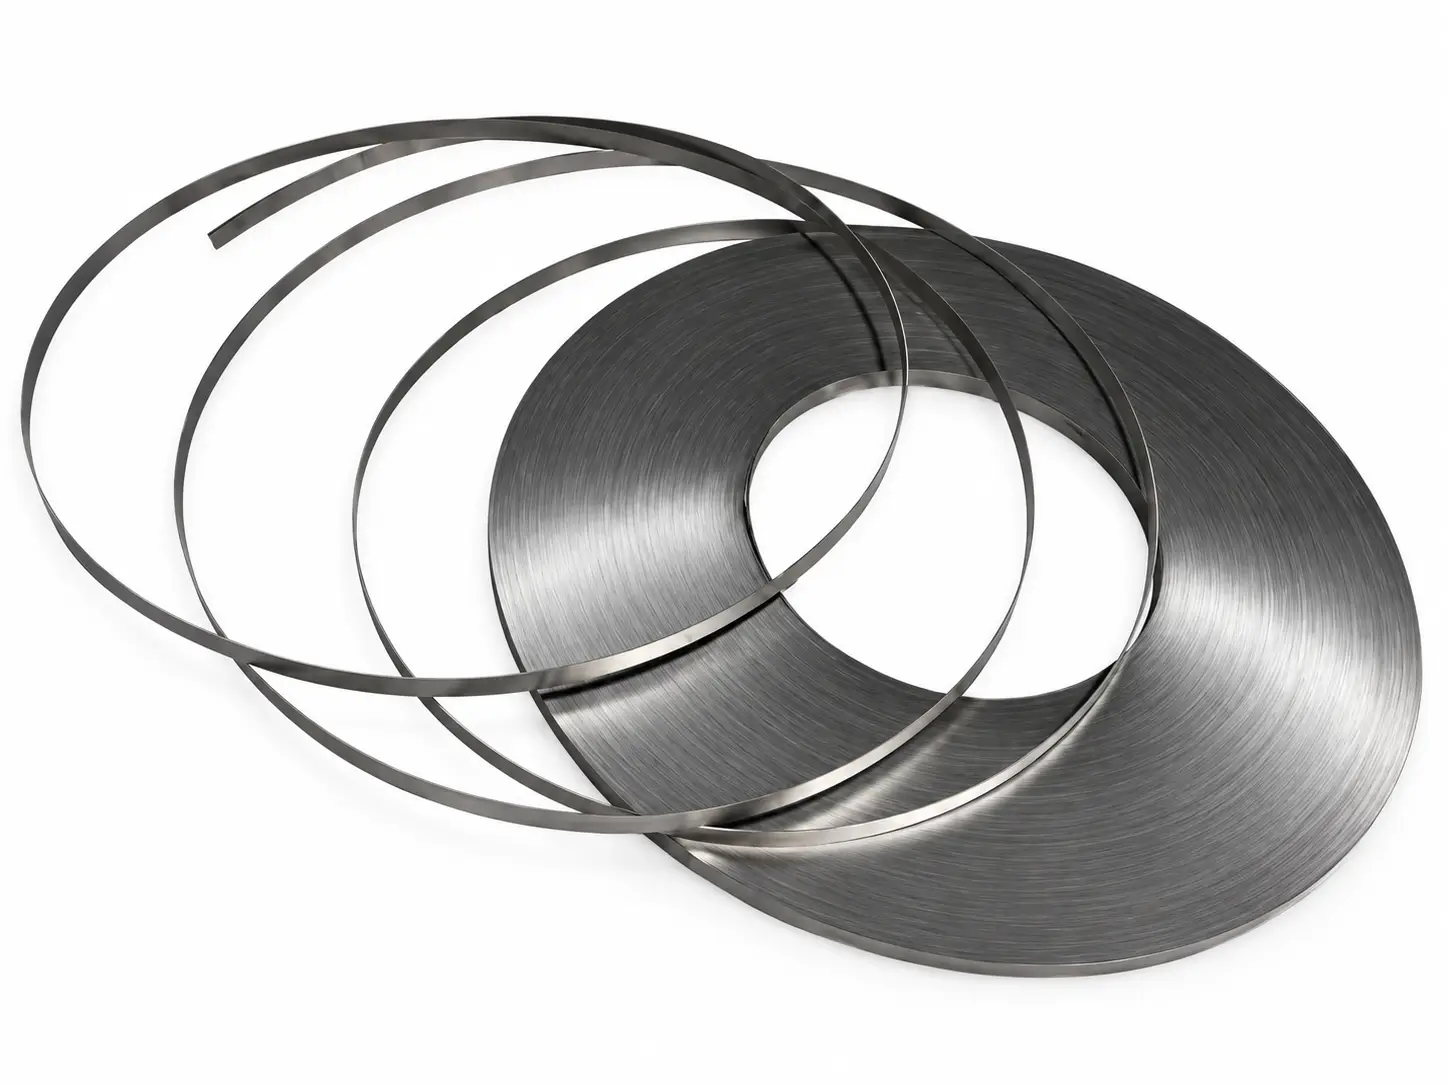
Flat continuous forms controlled by width, thickness, active length, spacing, supports and electrical feed.
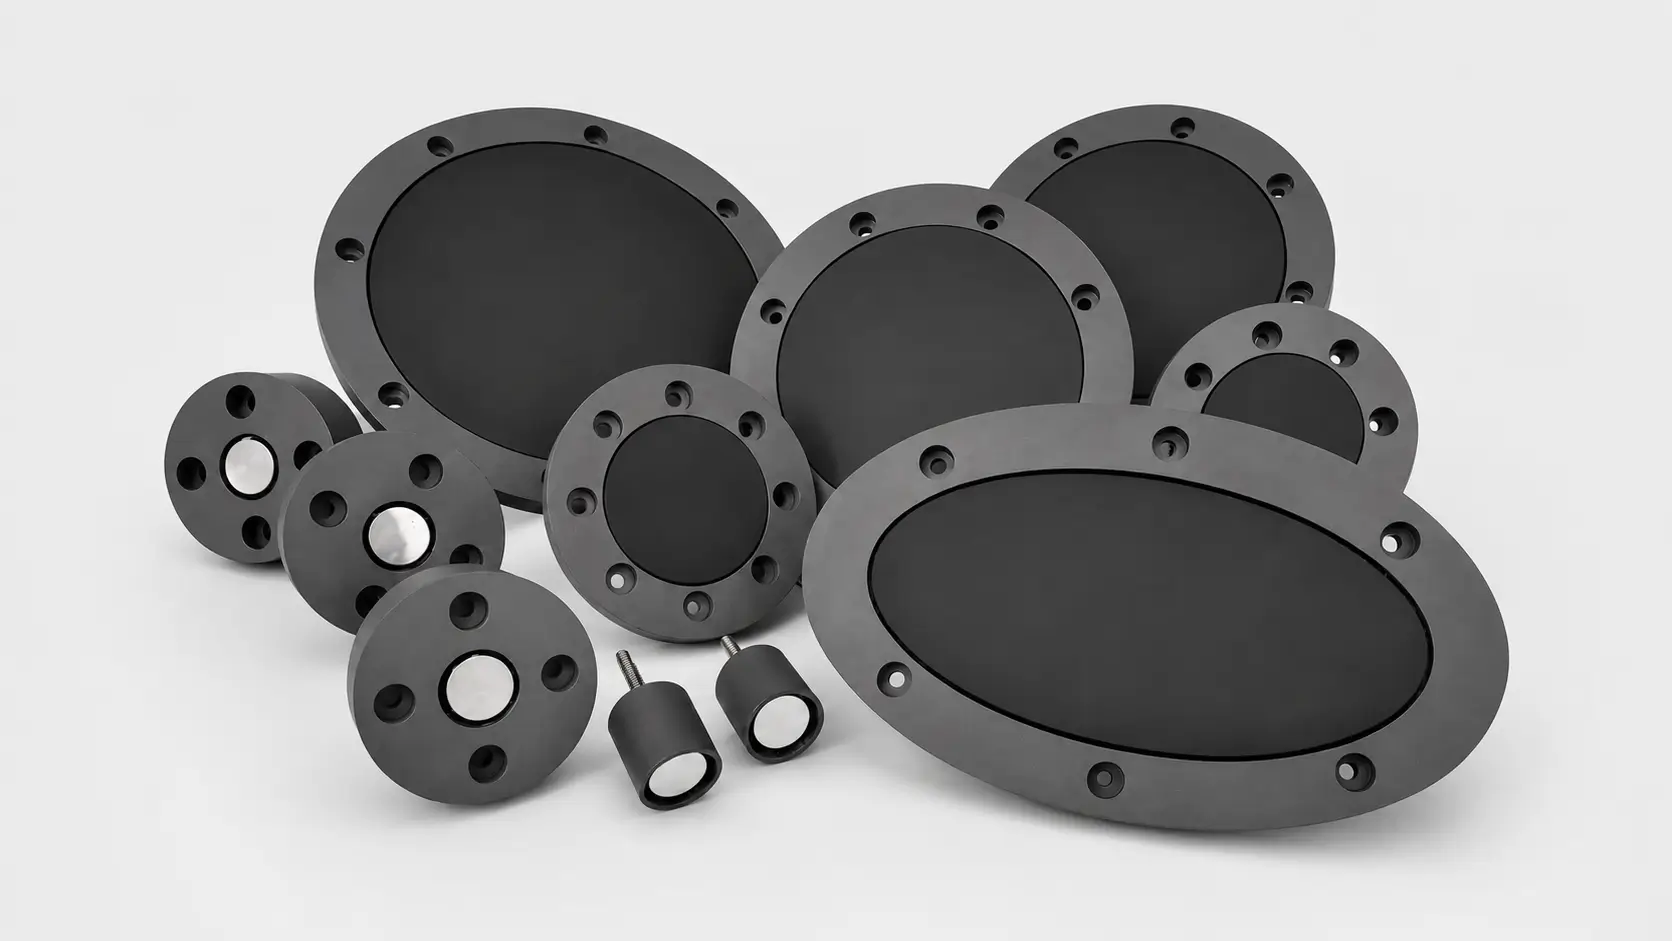
Localized or compact active faces requiring diameter/profile, coated face, edge mask, stem, seal and mounting.
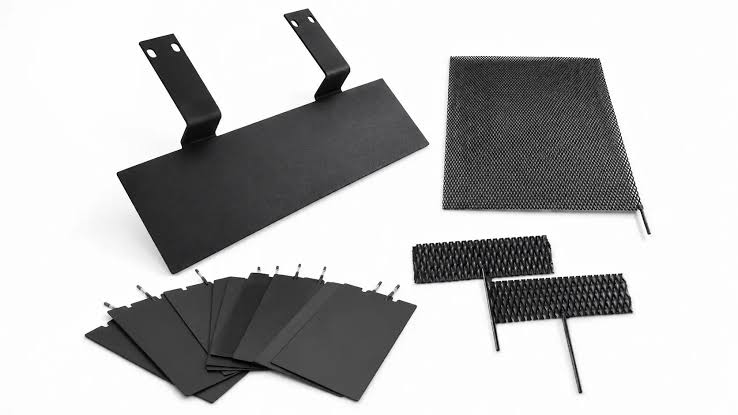
Custom structures with controlled frames, welds, active panels, feeds, contact areas, seals and replaceable interfaces.
Limits are order-defined because the coating, substrate exposure, current distribution and reaction environment interact. Declare fluoride, chloride and other aggressive or competing species instead of assuming one universal threshold.
Full bath, additives, metals, contaminants, cleaning and process changes.
Active area, gap, current distribution, gas release, scale and mass transfer.
Normal, peak, startup, shutdown, batch/continuous schedule and cooling.
Joint resistance, heating, seal, exposed titanium, mechanical damage and polarity.
No single test proves every coating property. Define each required characteristic and its method, sample, calibration, locations, units and acceptance.
Surface elemental composition under a calibrated plan; not automatic proof of total loading or thickness.
Use an agreed gravimetric, analytical, cross-sectional or validated method with a clear area basis.
Selected-sample morphology or phase information within method limits; may require destructive coupons.
Define test cell, reference, chemistry, temperature, duty, area basis and end point.
Accelerated conditions may support comparative qualification under an agreed method, but they do not directly guarantee field life without a justified correlation and matching operating basis.
| Direction | Starting duty | Do not assume |
|---|---|---|
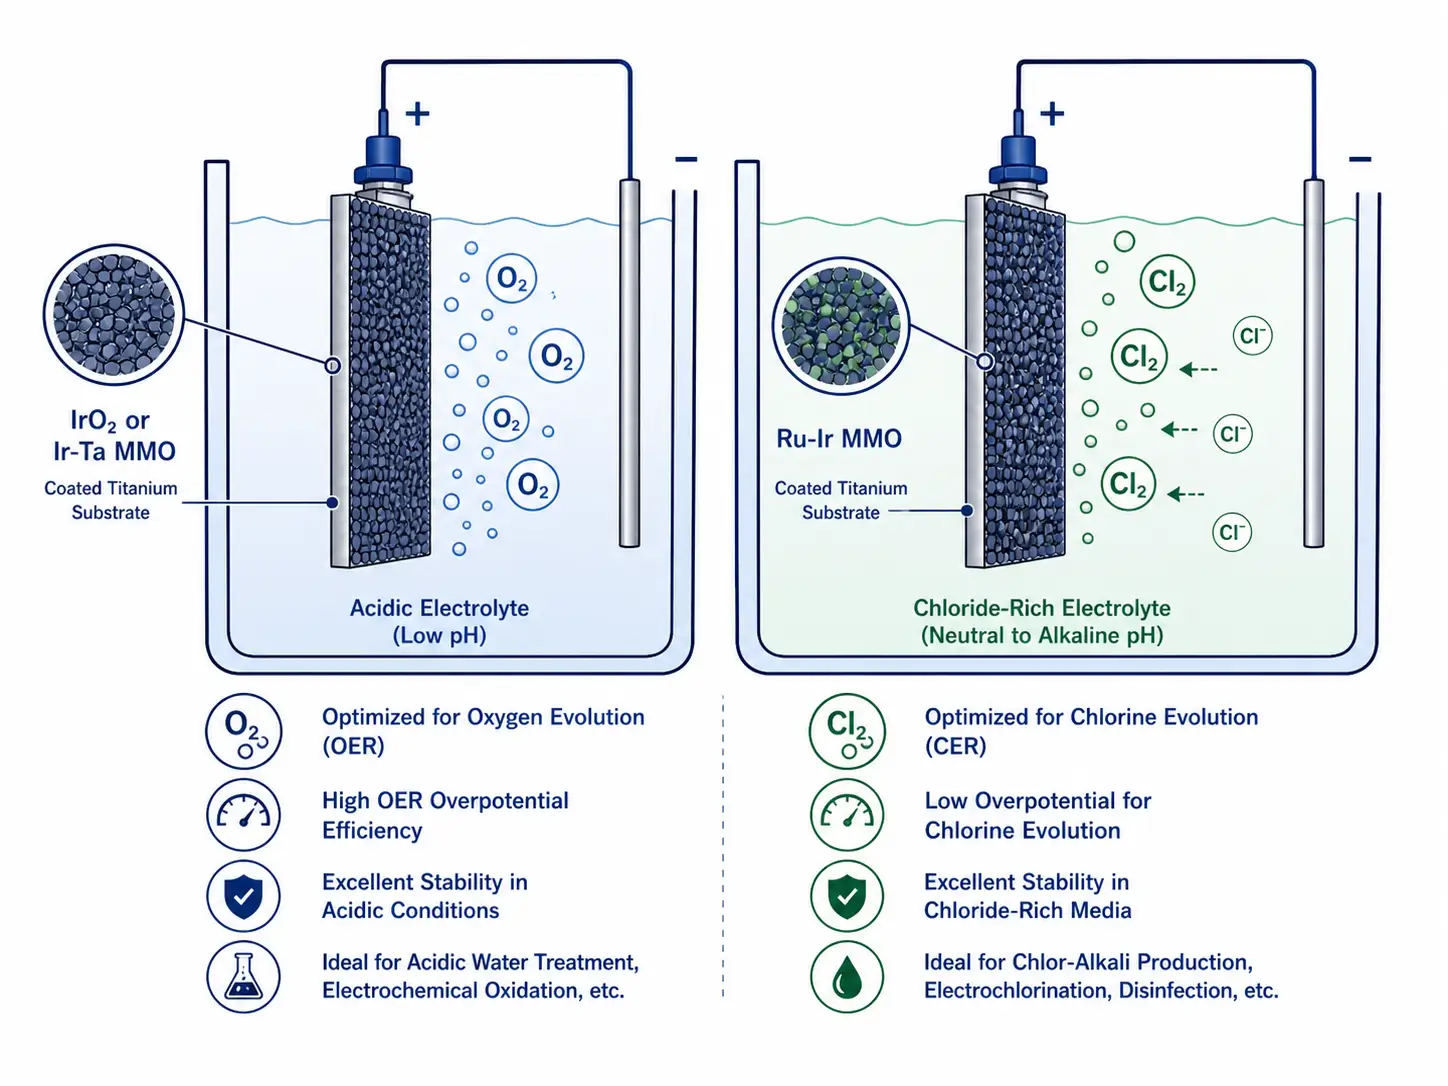
| IrO₂-rich / Ir-Ta MMO | Oxygen evolution under a defined electrolyte and electrical basis | All iridium coatings, baths and current densities are interchangeable |
| Ru-Ir MMO | Chlorine evolution under a defined chloride-process basis | Chloride presence alone proves the CER coating choice |
| Platinized titanium | Selected electrochemical duties reviewed from potential, chemistry, Pt basis and wear | Pt/Ti is automatically superior or equivalent in every OER process |
The applicable process route and evidence are confirmed against the approved coating requirement, active-zone drawing and inspection plan.
Confirm titanium form, material basis, heat/lot identity, geometry and drawing before preparation.
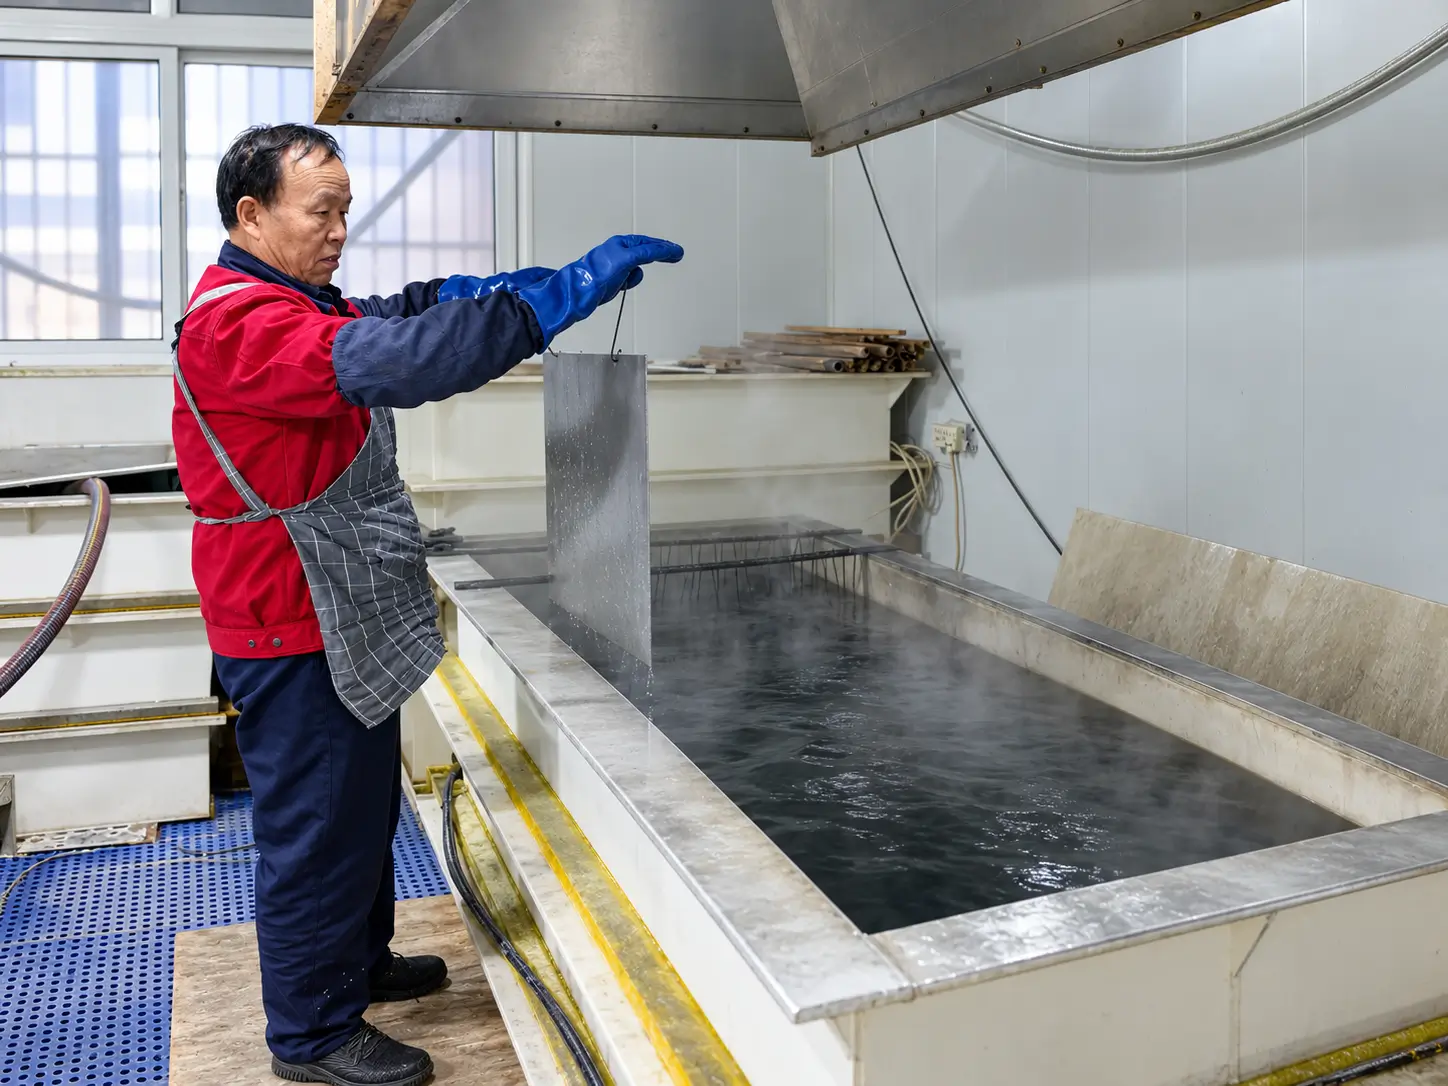
Control cleaning, activation, handling and the time/condition between preparation and coating.
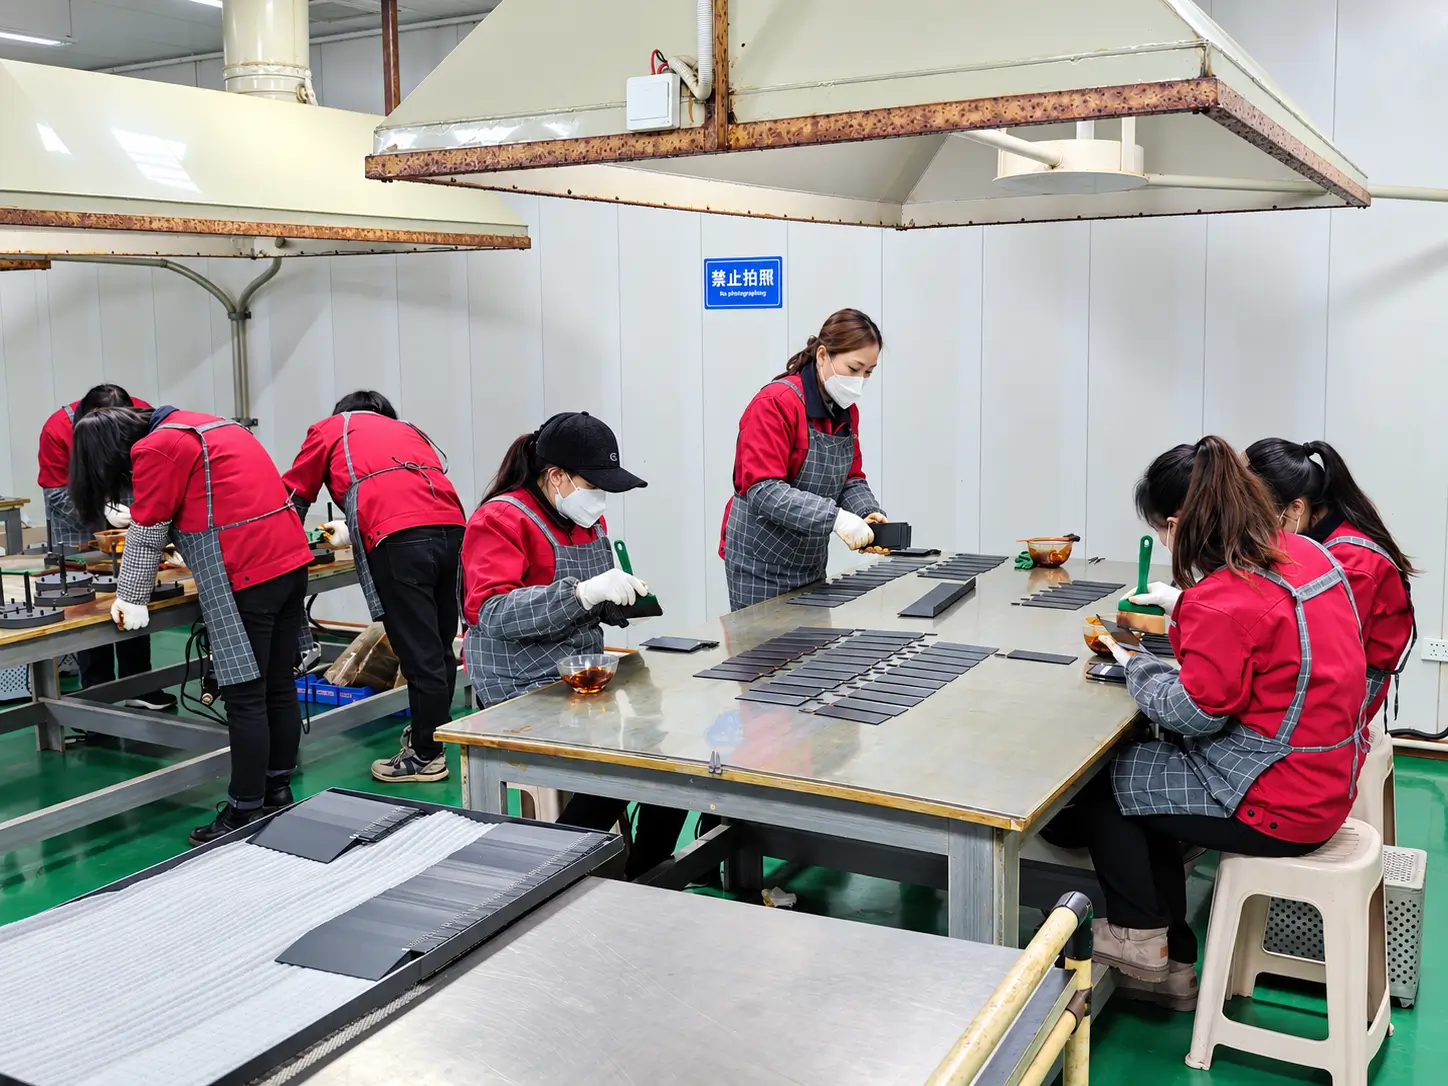
Apply the order-defined IrO₂-rich or Ir-Ta system to the approved active-zone map with batch/process records.
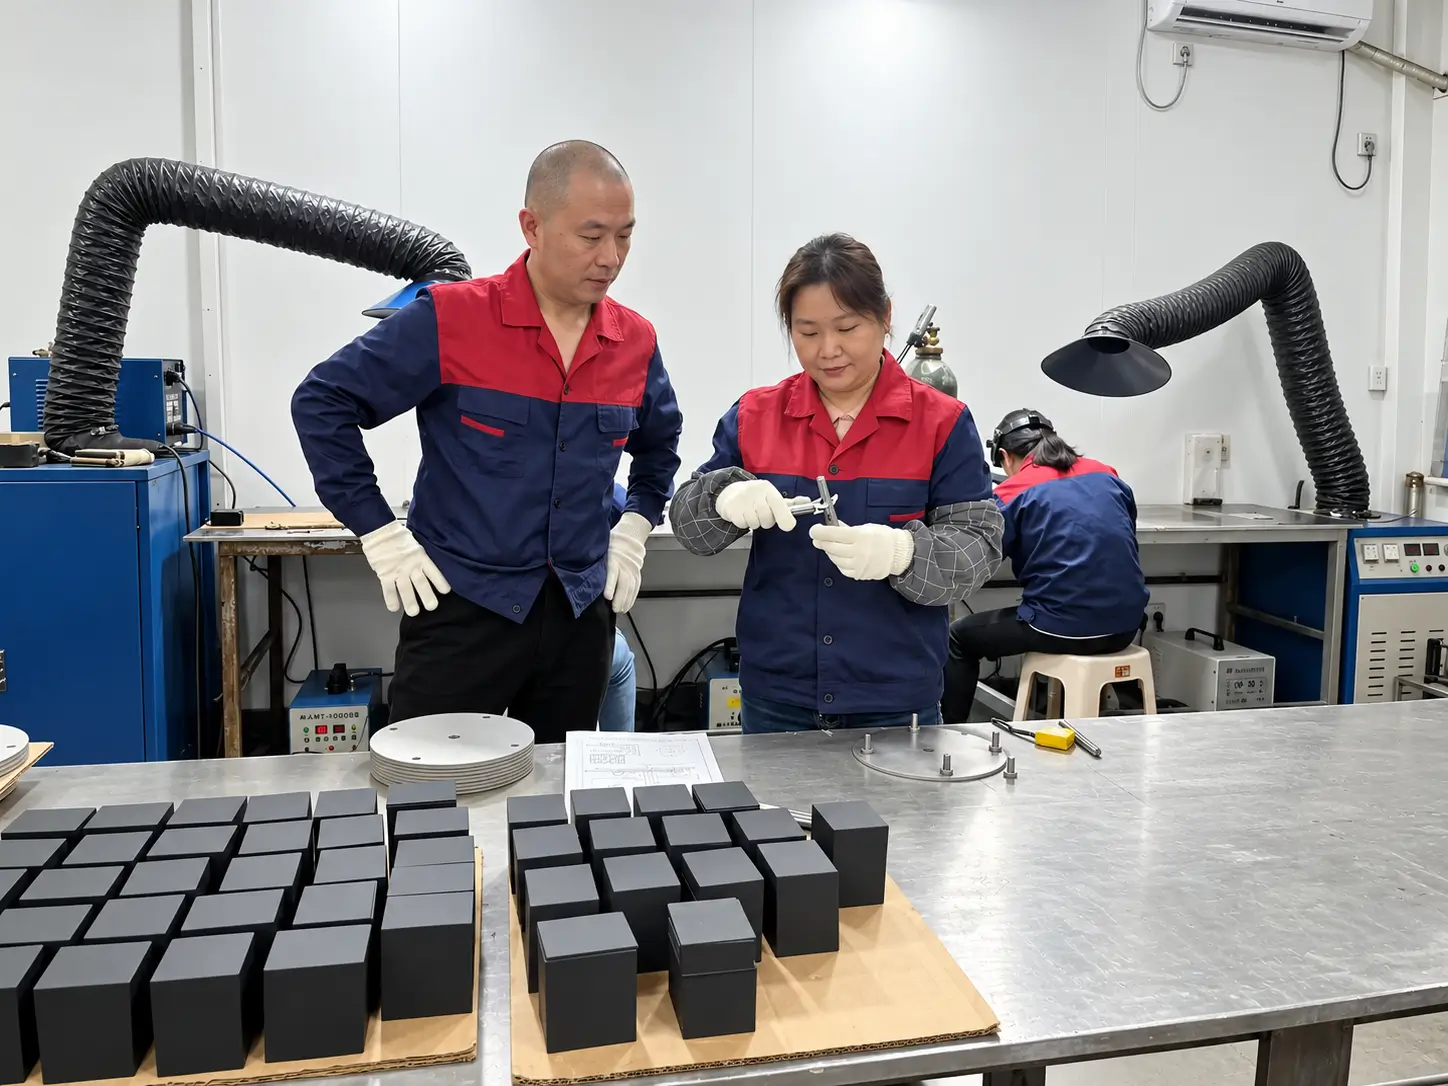
Verify agreed dimensions, coated/masked zones, connection and project-specific coating/electrical evidence.
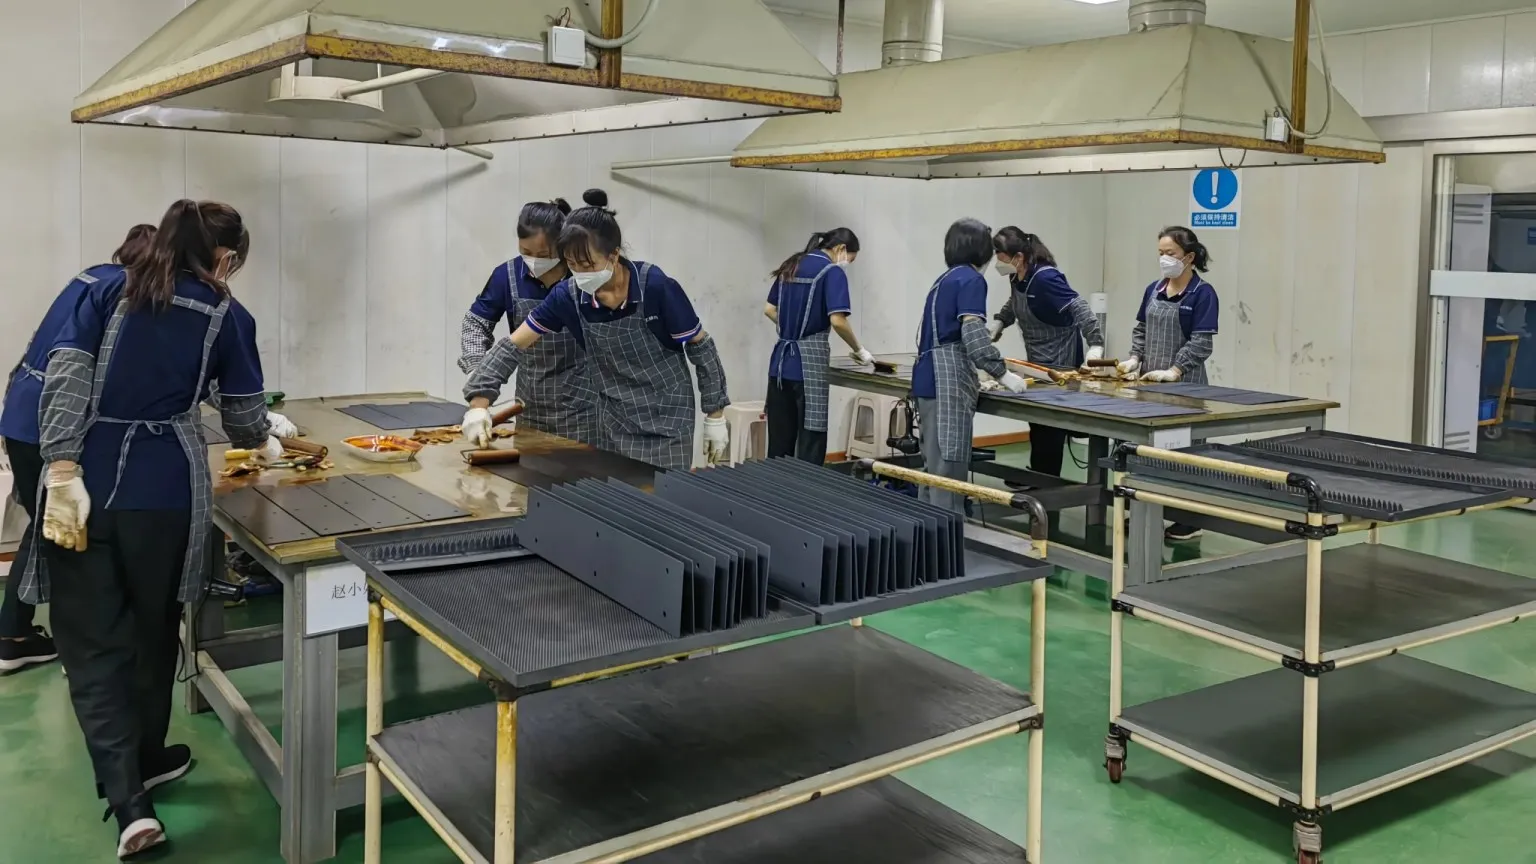
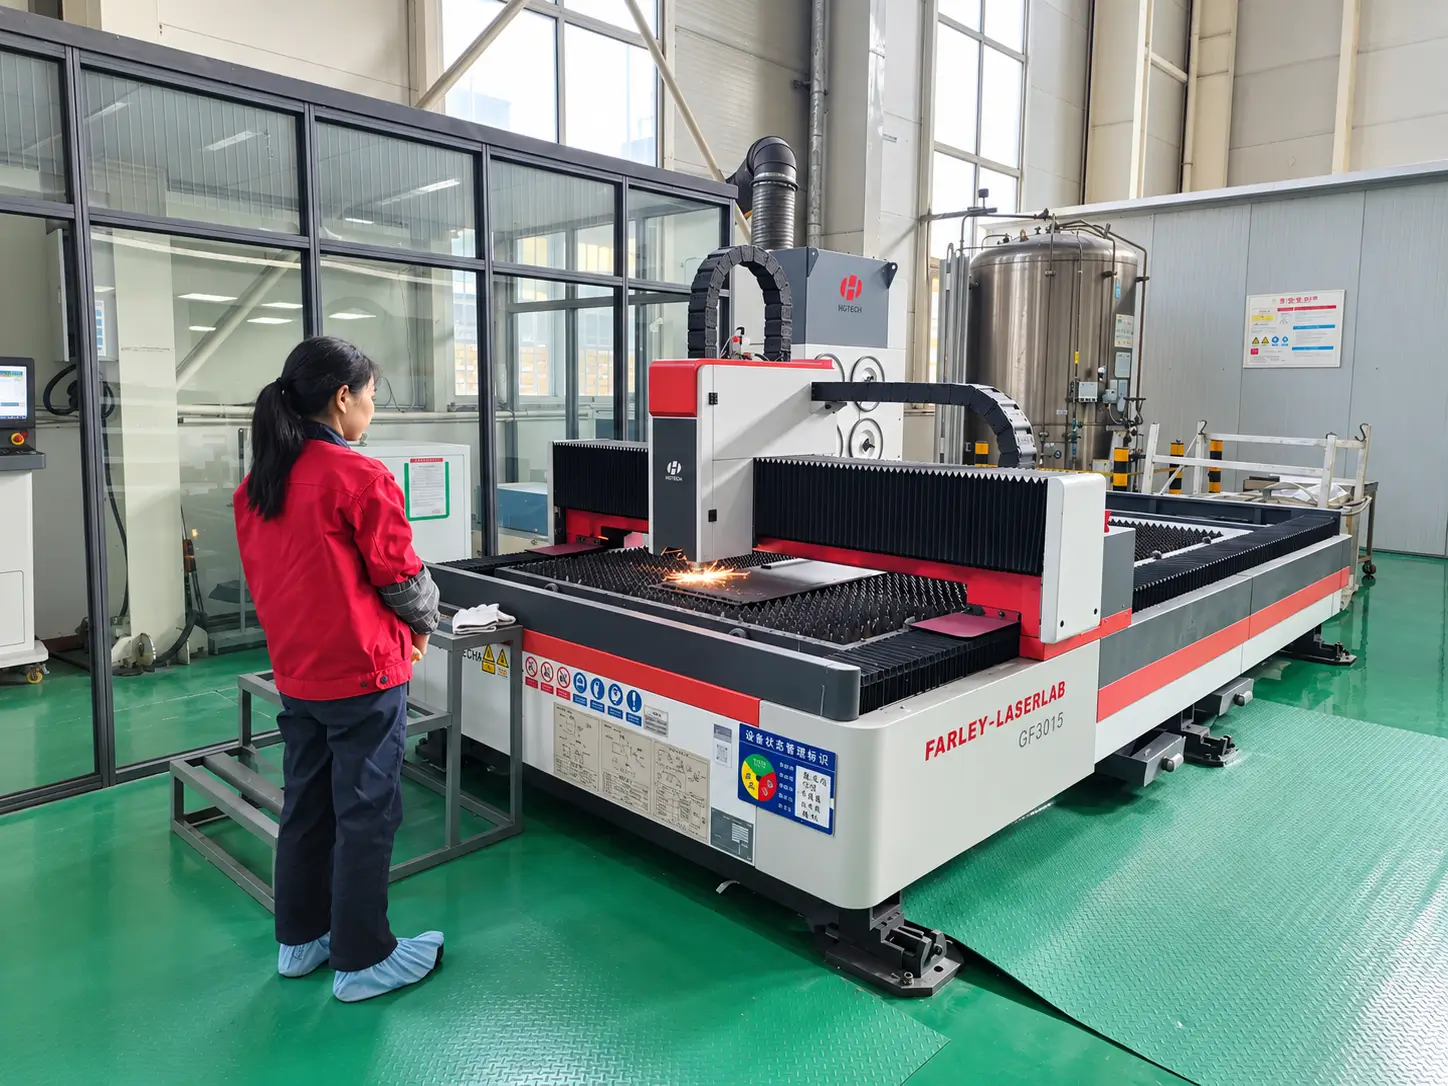
A concise view of HELE Titanium’s substrate preparation, coating, inspection and production environment.
Freeze the OER duty, bath chemistry, coating metric, active-area convention, current/voltage basis, geometry, connection, life method, evidence and system responsibility before issuing the order.
Reaction and process result
Electrolyte, contaminants and limits
Current, voltage and area basis
Coating, geometry and connection
Life, ALT and warranty boundary
Inspection, documents and exceptions
The Knowledge Center guide adds bath compatibility, test-method limits, installation, failure evidence, conditional recoating and quotation normalization.
Open the Iridium MMO Purchase GuideThese iridium-based MMO systems are commonly reviewed when oxygen evolution is the intended anodic reaction and the complete electrolyte, acidity, contaminants, temperature, current-duty basis and operating schedule are defined.
No. They are related iridium-based OER coating families, but composition, loading, processing and performance requirements should be defined separately for the actual electrolyte and duty.
No. Electroplating, electrowinning and acidic electrolysis cover different bath chemistries, additives, impurities, target reactions and electrical duties. The exact process window is required.
State total current and current density with the area denominator, active-zone drawing, normal/peak duty, voltage/reference basis, temperature, flow and electrode spacing.
Under a documented calibration and sampling plan, XRF may support surface elemental-composition assessment. It does not automatically prove total loading, thickness, adhesion, oxide phase, through-depth distribution or service life.
No. Voltage increase is a symptom. Review electrolyte, deposits, temperature, flow, current distribution, electrode gap, cathode condition, connection resistance and coating/substrate condition before identifying root cause.
A drawing, bath/process note or existing-anode record is enough to begin. Unknown items can remain open rather than being replaced by generic coating, current-density or life claims.
Prefer email?
sales@heletitanium.com