A dependable anode-basket order starts with the entire plating-line interface. Basket material and overall dimensions matter, but they cannot replace the bath, anode, electrical, structural, maintenance and inspection basis.
1. Confirm the Basket Role Before Selecting Material
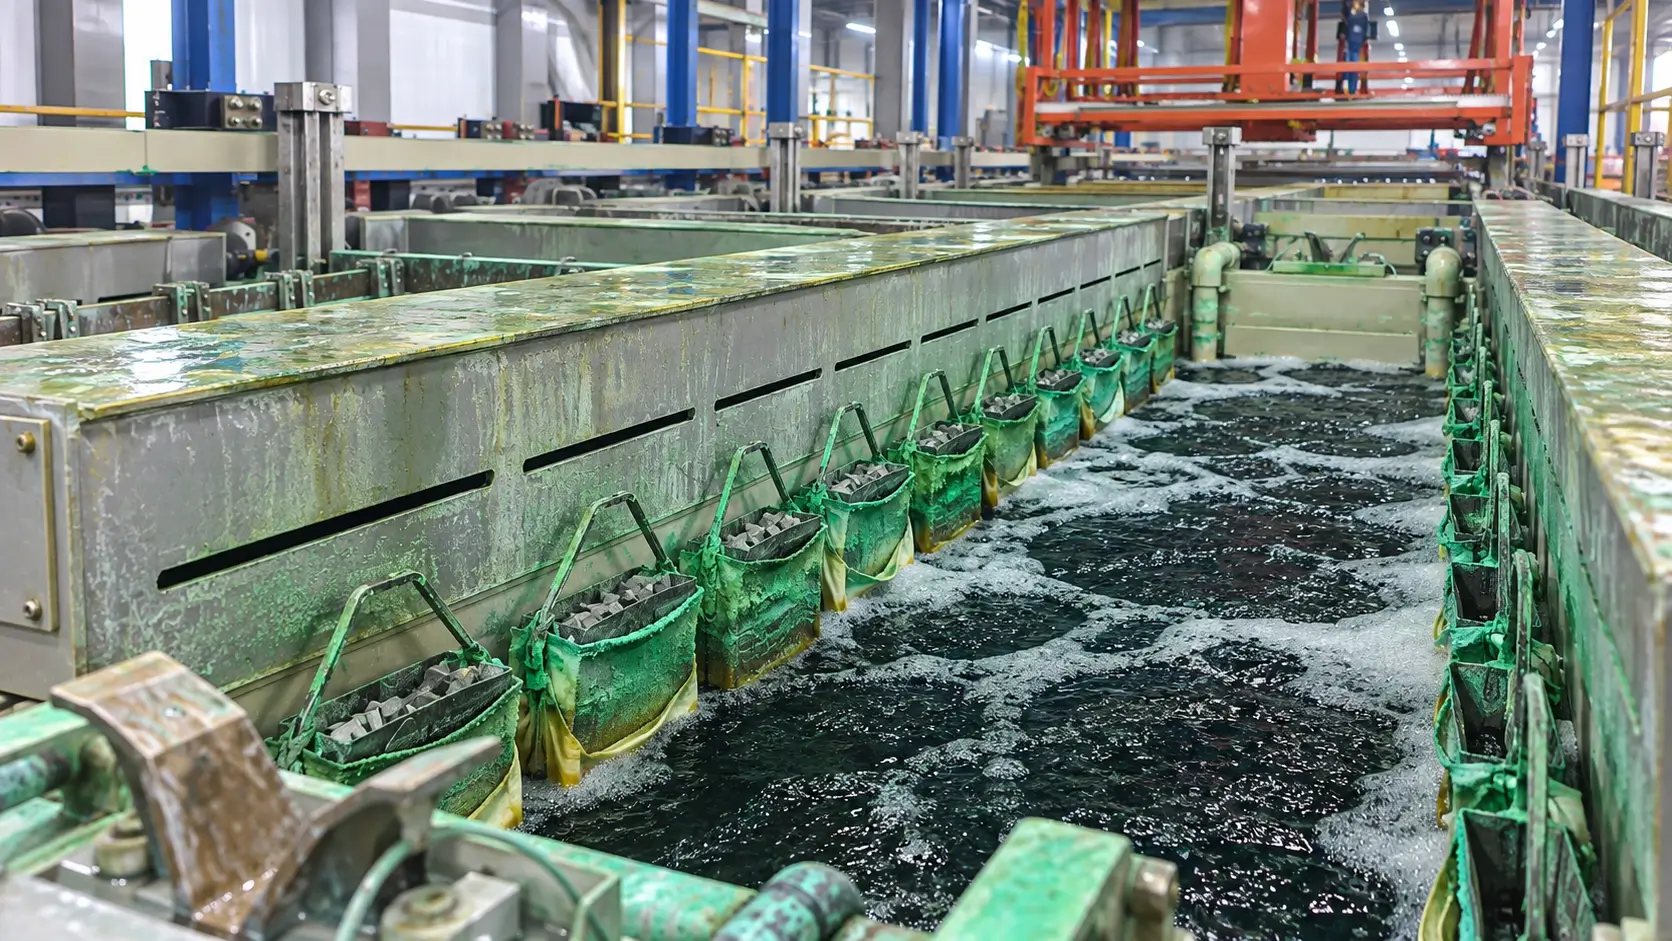
A titanium anode basket usually holds soluble metal anode pieces while carrying current from the busbar into that anode charge. It is not the same product as a work basket for carrying plated parts, a rack or jig, or an MMO/platinized titanium insoluble anode.
| Product role | Primary function | Do not confuse with |
|---|---|---|
| Soluble-anode basket | Contain anode metal, admit electrolyte and conduct current | Coated insoluble electrode |
| Work basket | Hold workpieces during processing | Anode carrier/current path |
| Rack / fixture | Position and electrically connect parts | Loose-anode container |
| MMO / Pt-Ti anode | Provide an insoluble electrochemical surface | Basket filled with soluble anode pieces |
2. Freeze Bath Chemistry and Material Compatibility
Provide the plating process or bath family, full chemistry where permitted, metal salts, acids/alkalis, additives, pH, concentration, operating temperature, contaminants, cleaning cycles and electrochemical conditions. Titanium is useful in many environments but is not universally resistant in every plating bath.
Fluoride-containing and other aggressive chemistries require explicit review. Do not approve a basket from the words “acid bath,” “nickel line” or “corrosion resistant” alone.
State the ordered Grade/UNS and each starting-material specification. ASTM B265 may apply to strip/sheet/plate, ASTM B863 to wire, and ASTM B348/B348M to bar or billet within their scopes. The approved drawing controls the finished basket.
3. Define Soluble Anode Material, Form and Loading
Identify anode metal/alloy, form, individual size range, fines, bulk behavior, initial and refill mass, target fill height, replenishment method and minimum operating level. Balls, pellets, chips, slabs and cut pieces can require different openings, containment and bag arrangements.
- Prevent the smallest intended anode piece from escaping through the basket.
- Review bridging, settling and electrical continuity as anode pieces dissolve.
- Define maximum wet and dry loads for the basket, hook and handling method.
- Provide refill access, cover or closure and safe handling requirements.
4. Coordinate Tank, Workpiece and Basket Geometry
Provide tank internal dimensions, liquid level, busbar size/location, workpiece envelope, anode-to-cathode spacing, basket quantity and position, agitation/flow features, nearby heaters/coils, shields, access and removal path.
For rectangular baskets state length, width and depth; for cylindrical baskets state diameter and length. Add hook position, immersion depth, bottom/side clearance, frame projection, bag envelope and installation tolerances. Replacement baskets should be controlled by a verified drawing rather than a sample photo alone.
5. Specify Expanded Mesh or Perforation Completely
| Construction | Minimum definition | Functional check |
|---|---|---|
| Expanded mesh | SWD, LWD, strand width, strand thickness, orientation, flattened/raised condition, open area | Anode containment, flow, stiffness, edges and bag fit |
| Perforated sheet | Hole shape/diameter, pitch, pattern, sheet thickness, open area, edge margins | Flow, containment, ligament strength and fabrication |
| Wire/rod grid | Wire/rod diameter, spacing, orientation, frame attachment and ends | Opening control, stiffness and weld/joint integrity |
| Mixed construction | Each material form plus joints and transitions | No unreviewed weak, sharp or electrically isolated areas |
There is no universal optimum open-area percentage. More open area can improve solution access but can reduce containment or stiffness; the final design must balance anode size, bag, structural load, current distribution, maintenance and bath operation.
6. Define the Busbar, Hook, Contact and Current Path
State busbar material, cross-section, orientation, coating/plating if any, basket quantity, total and per-basket current, duty cycle, contact arrangement, hook section/length/position, liquid level, joints, permissible temperature rise or resistance criterion where required, and maintenance/cleaning practice.
If a copper-cored titanium hook is proposed, define the conductor, titanium enclosure, joint/end closure, isolation of copper from the bath, inspection and repair rules. Do not assume this construction or a universal current rating.
A low-resistance hook does not by itself guarantee current distribution or plating uniformity. Rectifier settings, busbar, basket positions, anode loading, tank geometry, bath, agitation, workpiece/rack and operating controls all contribute.
7. Control Frame, Reinforcement, Welds and Handling Load
Define full basket weight, maximum anode charge, wet load, lifting and manual-handling method, unsupported span, impact or refill duty, frame sections, reinforcements, bottom and closure details. Identify critical welds/joints and any shielded welding, qualification, visual, dimensional or NDE requirements.
- Control sharp edges and snag points that can damage bags or operators.
- Review heat distortion and post-weld dimensions.
- Define whether the hook is a structural lifting point or electrical hanger only.
- State trial-fit or load-test requirements when project risk justifies them.
8. Treat the Anode Bag as an Engineered Interface
Specify bag fabric/material, chemical and temperature compatibility, dimensions, seam and closure, pore/retention or flow basis, expansion allowance, fit over frames/hooks, installation and replacement method. Identify anode fines/sludge behavior and cleanliness requirements.
A bag can help contain fines, but it does not guarantee bath cleanliness or deposit quality. Bag selection, filtration, agitation, maintenance and process control must work together.
9. Freeze Fabrication and Change Control
The route may include material cutting, expanding or perforating, forming, frame/hook fit-up, welding/joining, edge treatment, cleaning and assembly. The supplier should disclose the order-specific route and internal or externally controlled operations where qualification depends on them.
- Freeze drawing, BOM and inspection-plan revisions.
- Require written approval before changing Grade, material form, mesh/perforation, frame, hook/core, welding route or bag.
- Define first-article, sample, trial-fit and repeat-order controls.
- Record repair/rework, concessions and retest requirements.
10. Inspection, Traceability and Release Documents
| Control point | Possible evidence when required | Buyer decision |
|---|---|---|
| Material identity | MTC, Grade/specification, heat/lot link and identity transfer | Each material form matches the BOM |
| Geometry and fit | Overall dimensions, hook position, frame, liquid-level reference and trial-fit record | Basket installs and can be maintained |
| Mesh/perforation | SWD/LWD/strand or hole/pitch/pattern/thickness/open-area results | Containment and drawing criteria are covered |
| Fabrication | Visual/dimensional weld checks, PT or other NDE only where ordered | Method, extent and acceptance are defined |
| Electrical interface | Continuity/contact/resistance or load checks where specified | Test setup and limits match the approved design |
| Release | Document index, deviations, labels, packing list and photographs if required | Evidence links to shipped baskets |
EN 10204 3.1 identifies a document type. ISO 9001 is a quality-management-system standard. Neither replaces product-specific dimensions, electrical checks, fabrication evidence or process qualification.
11. Commissioning, Cleaning and Maintenance
Before production use, confirm installation, basket spacing, contact cleanliness, anode charge, bag fit, immersion level and current sharing under the line owner's approved procedure. Establish inspection intervals for contact wear, heating/discoloration, deformation, mesh damage, cracks/weld condition, bag damage, sludge/fines and anode bridging.
- Define compatible cleaning and deposit-removal methods.
- Do not abrade or chemically clean contact and basket surfaces without an approved procedure.
- Record repairs, replacements and changed operating conditions.
- Reassess the design after bath, current, anode form, workpiece or tank-layout changes.
12. Cost and Quotation Comparison
Cost can be driven by titanium Grade and material forms, basket dimensions, mesh/perforation tooling, frame/hook construction, conductor isolation, welding, edge treatment, bag, inspection, trial fit, quantity, packing and logistics. Compare the same technical scope rather than unit price alone.
- Normalize drawing revision, BOM, basket quantity and anode-load basis.
- Separate material, fabrication, hook/contact, bag, inspection, documents and freight.
- Record MOQ driver, quotation validity, schedule assumptions and exclusions.
- Compare replacement access, maintenance and usable delivered scope.
13. Complete Titanium Anode Baskets Purchase Guard
13.1 Product role and process
- Confirm soluble-anode basket rather than work basket or insoluble electrode.
- State plating process, bath, chemistry/conditions and responsible process authority.
- Identify workpiece, rack, rectifier and production-duty context.
13.2 Material and compatibility
- State Grade/UNS and specification/revision for sheet, mesh, wire, bar and hook parts.
- Review fluoride and other aggressive chemistry explicitly.
- Define substitutions and approval route.
13.3 Anode charge and loading
- State metal/alloy, form, size range, fines, initial/refill mass and fill height.
- Define refill, closure, bridging and minimum-level controls.
- Set maximum wet/dry basket load and handling method.
13.4 Tank and basket geometry
- Provide tank, liquid level, busbar, workpiece and obstruction data.
- State basket dimensions, quantity, position, spacing, clearances and access.
- Control all interfaces by approved drawing/revision.
13.5 Mesh/perforation
- Define SWD/LWD/strand or hole/pitch/pattern/thickness/open area.
- State orientation, edges, end containment and frame attachment.
- Match opening to anode size, flow, structure and bag.
13.6 Electrical path
- State busbar, hook/contact, joints, current/duty and liquid level.
- Define conductor/core isolation where applicable.
- Agree electrical inspection, cleaning and maintenance criteria.
13.7 Frame, welds and bag
- Define frame/bracing, critical joints, weld inspection and load basis.
- Specify bag material, dimensions, seam, closure, retention/flow and change-out.
- Eliminate sharp or snagging edges.
13.8 Inspection and evidence
- For each characteristic state method, extent/sampling, acceptance and report.
- Link materials, basket ID, drawing, results, deviations and packing list.
- Define first article, witness or third-party inspection only where required.
13.9 Commercial and change control
- Normalize quantity, MOQ, currency, validity, Incoterm and named place.
- Separate basket, hook, bag, tests, documents, packing and freight.
- Require written approval for material, geometry, route and source changes.
13.10 Packing and delivery
- Protect hooks, frames, mesh, edges and bag-contact surfaces from distortion.
- Separate items by ID, drawing revision, Grade/heat and inspection status.
- Align labels, packing list, drawing and document index.
Red flags before purchase order
No exact chemistry, temperature or electrochemical compatibility review is stated.
SWD/LWD/strand or hole/pitch/pattern and measurement method are missing.
Busbar, contact, joints, duty, temperature and maintenance are not defined.
A quality-management-system standard replaces basket-specific evidence.
Decision gate
Do not release the order until process, bath, anode, material, geometry, mesh/perforation, current path, structure, bag, inspection, maintenance, documents and commercial terms describe the same deliverable.
14. RFQ and Pre-Order Checklist
Bath chemistry/conditions, workpiece, soluble anode metal/form and operating duty.
Tank, liquid level, busbar, basket quantity/position, spacing and access.
Type, dimensions, Grade/BOM, mesh/perforation, frame, load and drawing.
Current/duty, hook/contact, conductor isolation, bag and maintenance.
MTC, dimensions, mesh/perforation, weld/contact checks and traceability.
Quantity, MOQ, packing, destination, Incoterm, required date and exclusions.
15. Titanium Anode Baskets Purchasing FAQ
Which titanium Grade is commonly considered for anode baskets?
Commercially pure titanium such as Grade 1 or Grade 2 is often reviewed, but the final Grade and product form must follow the exact bath chemistry, temperature, electrochemical conditions, structural load and purchase specification.
What standards may apply to the starting material?
ASTM B265 can apply to titanium strip, sheet and plate; ASTM B863 to titanium wire; and ASTM B348/B348M to bar or billet within their scopes. The finished basket still needs an approved drawing, fabrication requirements and inspection plan.
How is basket current capacity determined?
It cannot be selected from basket dimensions alone. Review total and per-basket current, duty cycle, busbar/contact design, hook section, joints, titanium current path, contact resistance, temperature rise, bath conditions and maintenance.
How much open area should the basket have?
There is no universal percentage. Open area must balance electrolyte access, anode-particle containment, structure, current distribution, bag fit and service life. State the selected mesh/perforation geometry and acceptance method.
What should be checked on a copper-cored titanium hook?
If this construction is used, define the conductor, titanium cladding or sleeve, end closures, isolation of copper from the bath, joint details, current path, inspection and maintenance. Do not assume every hook uses this route.
How should two basket quotations be compared?
Normalize bath/process basis, basket type, Grade and material forms, dimensions, mesh/perforation, frame, hook/contact, loading, bag, fabrication, inspection, documents, quantity, packing, Incoterm, schedule assumptions and exclusions.