The most important line on a titanium-clad copper drawing is often the liquid line. A conductor can have the right copper core and titanium jacket, yet fail the project if a drilled hole, cut end or terminal exposes copper where process liquid can reach it.
Copper provides the current-carrying path; titanium is selected for exposure to the specified environment. The finished assembly’s behavior still depends on the cross-section, bond, connections, cooling and every place the protective layer ends. Material names alone do not settle those design choices.
The short answer: Provide an electrical and exposure map. Then define composite form, copper and titanium material requirements, core and jacket geometry, exposed or sealed regions, connection details, operating conditions and the tests for the delivered assembly.
1. What is the composite expected to do?
Titanium-clad copper is usually chosen to combine a copper current path with a titanium outer surface in a specified corrosive or electrochemical environment. That description is a design concept, not a blanket corrosion or current rating. A correctly chosen titanium grade may perform well in one process and be unsuitable in another; an adequately sized copper core can still be limited by contact resistance or temperature rise at a joint.
The buyer should therefore begin with two maps. One traces current from the power connection through the conductor and into the working component. The other shows immersion, splash, vapor, condensation and dry zones. Put them on the same drawing. Where those maps cross—at a terminal, clamp, drilled hole or cut end—the design needs a deliberate exposure and sealing decision.
Fastest way to avoid an expensive mistake: mark every place copper is intentionally exposed and every place it must remain protected. Then specify how each transition is made, inspected and maintained.
2. Which form should be quoted?
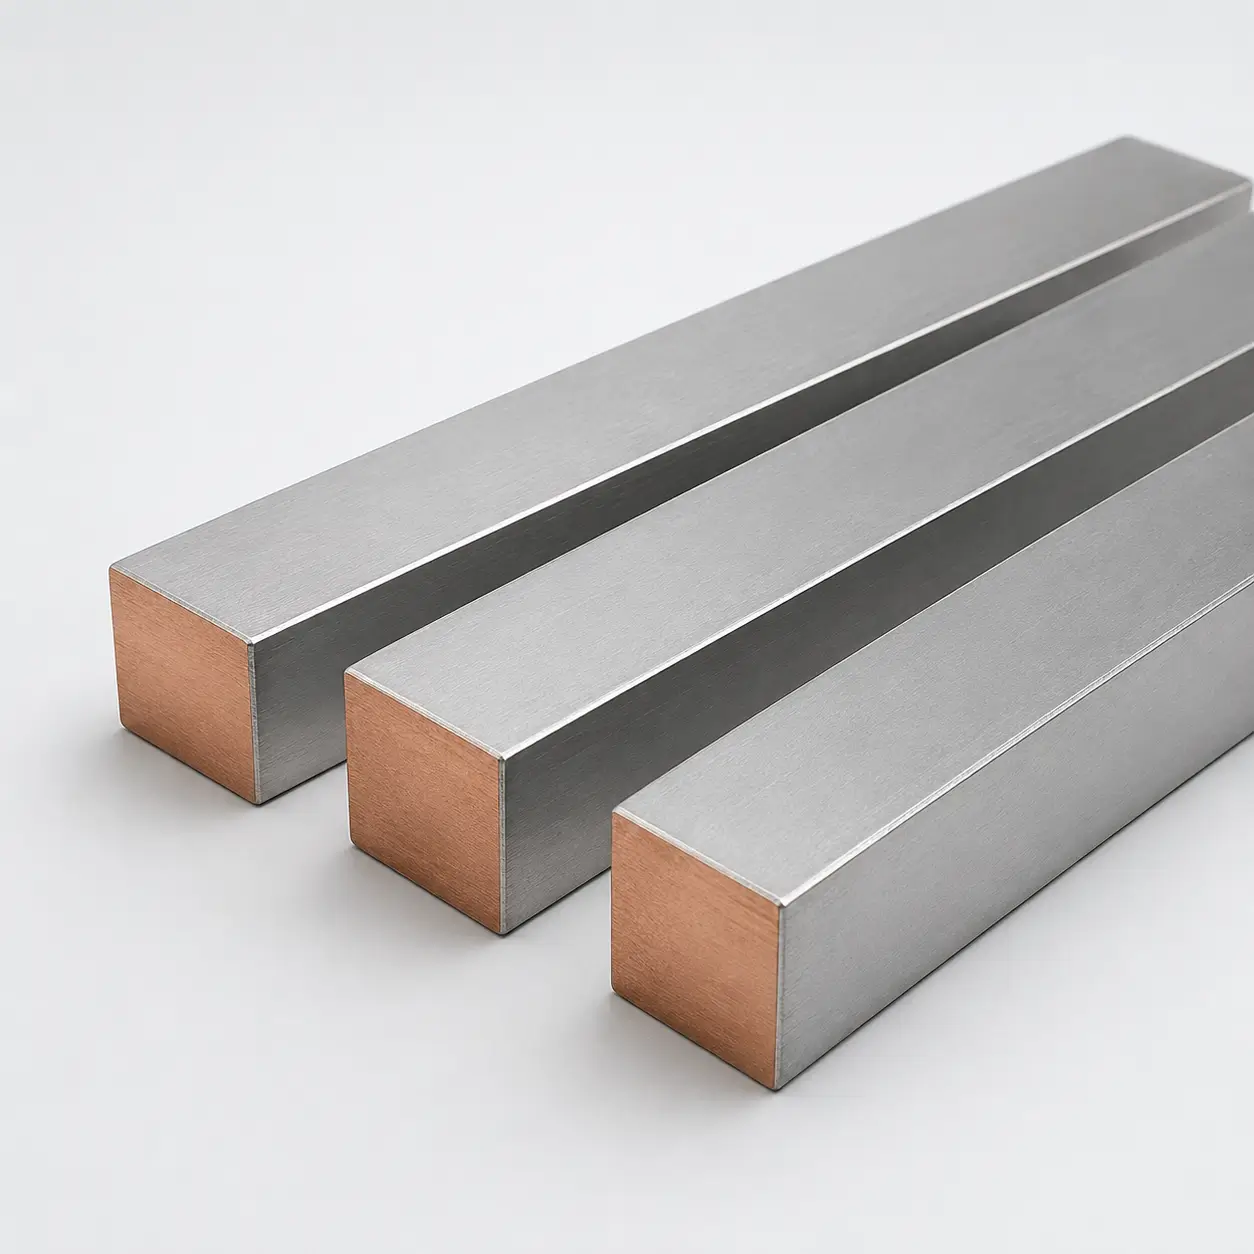
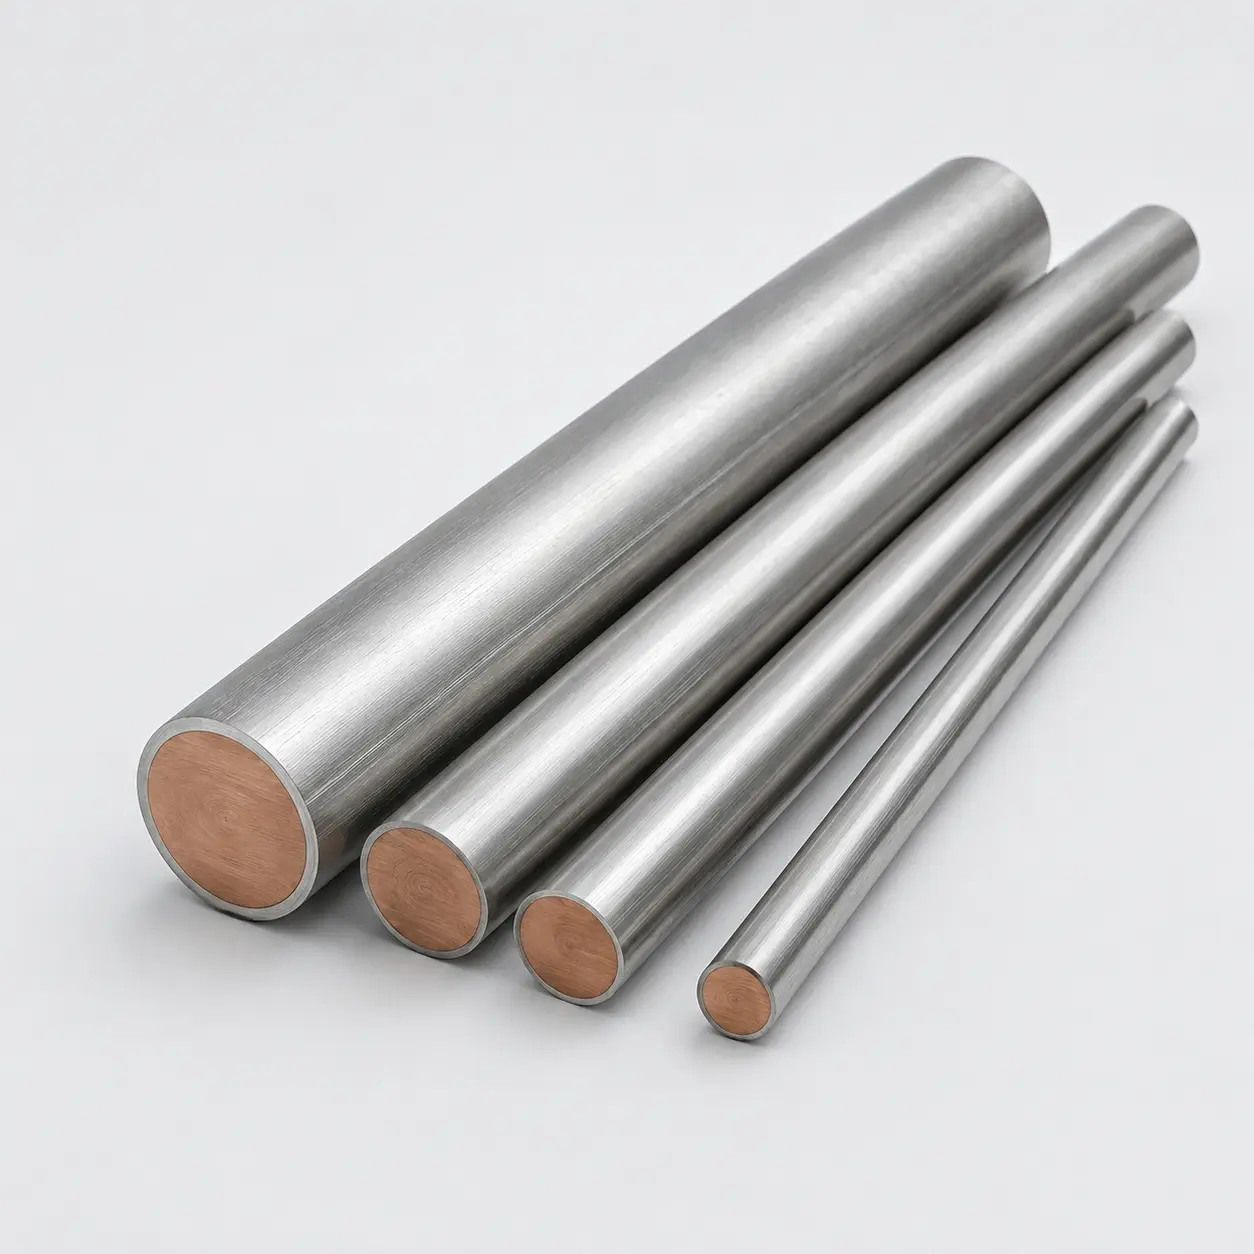
Round rod, rectangular bar, busbar and clad plate do not share one universal manufacturing or test route. A drawing should identify the delivered form and whether HELE is quoting raw composite stock, a cut blank or a finished conductor with machined terminals and seals.
| Form | Common design question | Quotation boundary |
|---|---|---|
| Clad rod | What are the core diameter, overall diameter and end transitions? | Stock length versus threaded or machined terminal. |
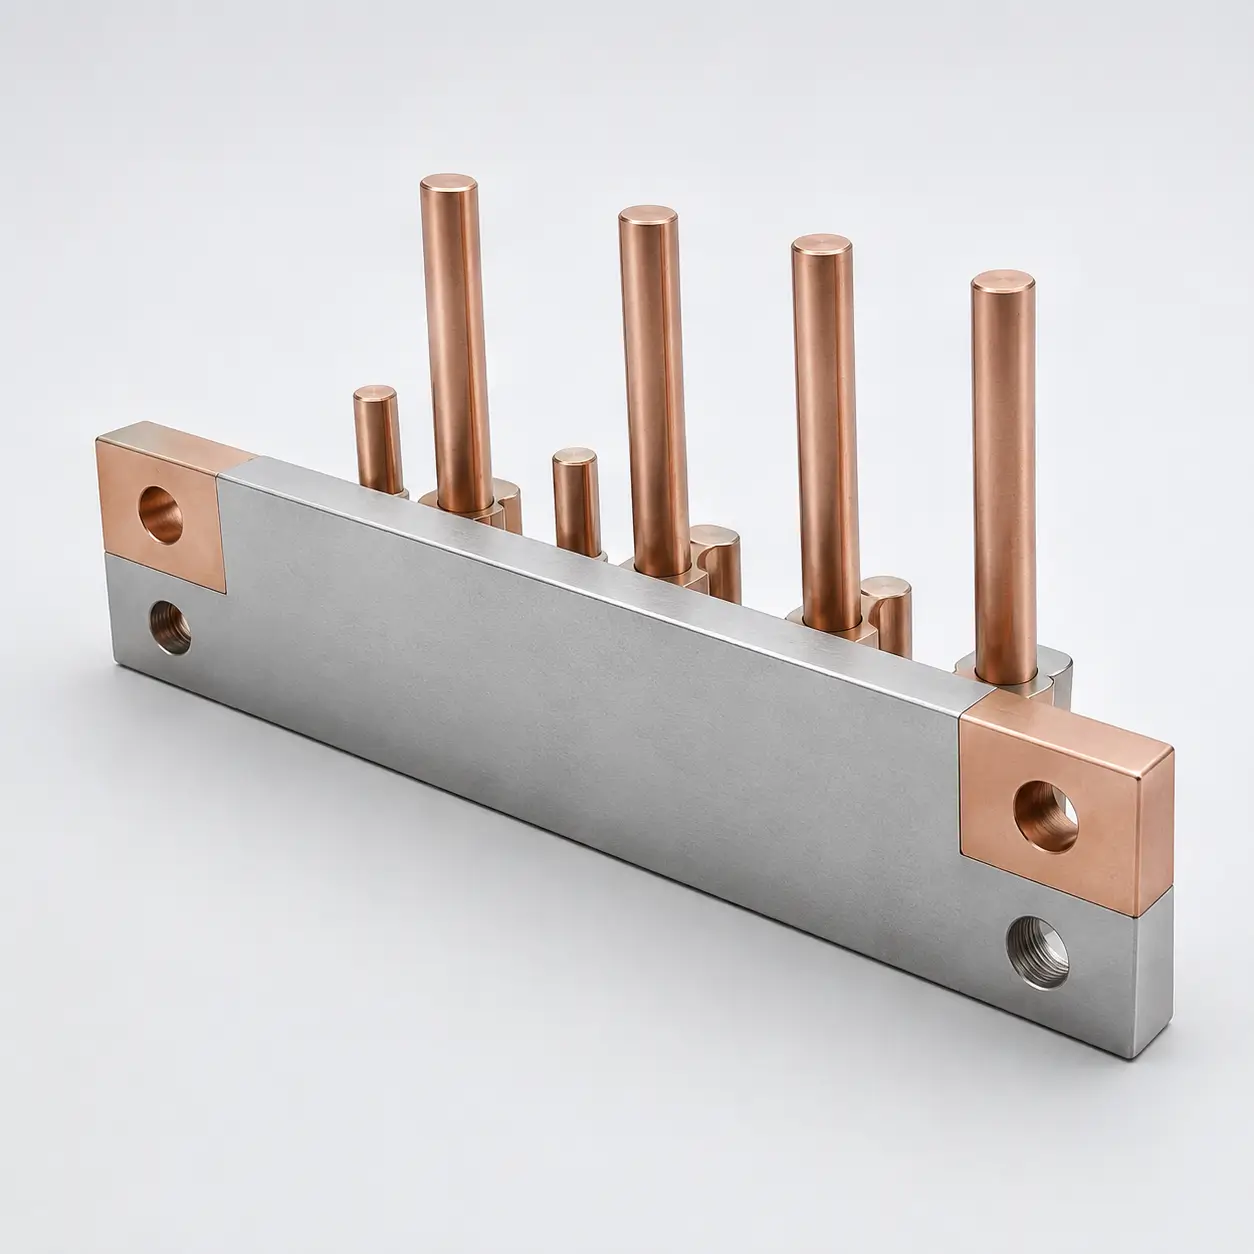
| Clad bar or busbar | How are cross-section, holes, contact faces and support loads arranged? | Bar stock versus drilled, bent or joined assembly. |
| Clad plate/strip | Which side is clad, and what happens at edges and cutouts? | Plate material versus a fabricated part or cell component. |
| Custom connector | How are dissimilar contacts sealed and electrically joined? | Composite material versus a qualified connection design. |
Do not accept “titanium-clad copper” as a sufficient product standard. ASTM B898 addresses reactive-metal-clad plate within its scope; it is not a general rod or busbar standard. Copper conductor bar may be specified to an applicable ASTM B187/B187M route, and titanium feedstock may have its own standard. Those constituent-material documents still do not define the finished bond, end seal, resistance or assembly dimensions.
Ask each supplier to identify the actual composite route and applicable product or project specification for the form offered. The buyer does not need a vague list of every possible bonding method; it needs the method proposed for this geometry and the evidence that the delivered lot will meet the agreed acceptance plan.
3. Where can process liquid reach the copper?
The titanium-covered length is only part of the exposure story. Cut ends, drilled holes, threads, grooves, bends and contact surfaces can interrupt the jacket. Some copper exposure may be intentional in a dry electrical cabinet. The same detail can be unacceptable below the liquid line or in a splash zone. The design must show which is which.
- Immersed zone: show the required titanium coverage, any penetrations and the allowable inspection access.
- Splash and vapor zones: include intermittent wetting, condensate and cleaning exposure rather than labeling the whole area “dry.”
- Dry terminal zone: define exposed copper contact faces, fastening method, electrical contact pressure and protection from accidental wetting.
- Transitions: detail where the jacket stops and how the end or hole is sealed or otherwise protected.
HELE’s titanium-clad copper product range includes several forms, but an order-specific drawing should decide the exposure boundary. Without it, two suppliers can price apparently identical rods while one includes machined and sealed ends and the other supplies open stock.
Corrosion language needs service conditions
A titanium surface is not “chemically immune” in every medium. Composition, temperature, contaminants, electrochemical potential and crevices can change suitability. Share the electrolyte or process chemistry, duty cycle and cleaning procedure with the design authority and supplier. Where the material choice is controlled by the customer specification, any alternate titanium grade or exposed-copper detail needs approval before ordering.
4. How should electrical and thermal duty be specified?
“High conductivity” is too general to design a conductor. Give normal and peak current, duration, permitted voltage drop, ambient and process temperatures, cooling, conductor length and contact arrangement. The electrical path includes the copper core, the composite transition and all contacts. A copper-core conductivity figure is not the measured resistance of the finished assembly.
Cross-sectional area and length influence resistance, but heat rejection and contact condition influence temperature rise. A busbar with a large core can still run hot at a poor contact. A thin titanium skin may protect the designed wet zone but leave a vulnerable terminal if the liquid line moves. The engineer of record should set the electrical and thermal acceptance criteria; the supplier can then quote dimensions, materials and any agreed resistance or temperature checks.
For a new design, ask whether the most useful acceptance test is constituent copper conductivity, finished-part resistance between defined terminals, or both. State the measurement temperature and contact locations. If current distribution into an electrode or hanger is critical, a simple end-to-end resistance may be necessary but not sufficient; system testing may still be required.
5. How will the bond and connections be accepted?
“Fully bonded” needs a test method and acceptance level. Depending on form and project, inspection might include visual cross-sections, ultrasonic examination, mechanical tests or another agreed method. Each has limits. An ultrasonic report should identify scan coverage and reportable discontinuities; it does not prove a universal “zero delamination” outcome.
| Feature or test | What it can answer | What remains to specify |
|---|---|---|
| Constituent certificates | Are the copper and titanium materials the ordered grades? | Standards, heat/lot and mapping into the composite. |
| Bond examination | Is the interface accepted within the agreed method? | Coverage, acceptance and which stage is tested. |
| Finished dimensions | Do clad thickness, overall section and terminal features meet drawing? | Measurement locations and post-machining state. |
| Electrical measurement | Does the finished path meet a defined resistance or voltage-drop criterion? | Test points, temperature, current and contact setup. |
| Seal and exposure check | Are intended dry and wet zones as drawn? | End/penetration detail and inspection method. |
Machining can remove titanium and reveal copper. Holes and slots may also interrupt the bond region. Specify whether those operations happen before or after bond inspection, and what is checked on the finished part. If a connection is assembled on site, split factory and site acceptance responsibilities so neither side assumes the other has tested the completed current path.
Test the connection as a component, not only its materials
A copper certificate and a titanium certificate are necessary for material identity when specified, but they do not describe the resistance of the assembled terminal. If a site will bolt the conductor to another bar, contact finish, fastener, clamping force and future access become part of the electrical design. The buyer should define whether factory acceptance ends at the bare contact face or includes a bolted test joint. The result cannot be compared unless the test setup matches the quoted scope.
For immersed applications, a terminal or hole may also be a corrosion path. A cross-section or other agreed examination can demonstrate local coverage in a sample; production inspection then needs a defined method and frequency. The inspection plan should target the transitions that could fail, rather than relying on a bond test performed far from the working end.
6. Why do offers differ in price and responsibility?
The material proportions, bonding route, shape, machining, sealing, inspection and document scope all affect price. A bare clad rod may appear cheaper than a conductor with finished terminals, but the buyer must then add machining and qualification. A long busbar can use more copper while reducing joints; a shorter design may save material but add contact losses and assembly work. Neither comparison is resolved by price per kilogram alone.
Ask for a stage-by-stage quote: constituent materials, composite stock, machining and forming, terminal and seal work, bond inspection, electrical checks, documentation and packing. Also ask who performs each process and who releases the finished item. Do not assume that a material standard or a broad “manufacturer” label establishes a specific factory, joining method or test coverage.
Availability, maximum size, bond-process route, MOQ and lead time depend on the particular form and drawing. HELE should confirm those details in the offer rather than turning an isolated past capability or product photograph into a site-wide promise.
7. What should the RFQ contain?
- Application and complete current path: normal/peak current, duty cycle, allowable loss and thermal conditions.
- Process chemistry and a marked immersion, splash, vapor and dry-zone map.
- Conductor form, drawing, copper and titanium grades/standards, core and jacket dimensions.
- Every cut end, hole, contact face and seal, with factory versus site assembly boundaries.
- Bond, dimensional, resistance and material-traceability acceptance requirements.
- Quantity, repeat demand, delivery stage and destination.
If the project is a replacement, include the old drawing and photographs of the failed or removed part where permitted. Mark any field changes in liquid level, contact design or cleaning practice. Copying an old conductor without understanding those conditions can repeat the same failure mode.
Questions buyers often ask
Does copper-core conductivity equal finished conductor conductivity?
No. Finished resistance also depends on geometry, transitions and contacts. Specify which property is tested and the method.
Does ASTM B898 cover titanium-clad copper rod and busbar?
Its published scope concerns reactive-metal-clad plate. A rod or busbar needs an applicable project/product specification and finished-composite acceptance plan.
Can a bond test prove there will be no delamination in service?
A test supports acceptance within its coverage and criteria. Service performance also depends on loading, temperature, geometry, corrosion exposure and the assembled connection.