A coil can be the right alloy and gauge yet be unusable on the buyer’s line. It may be too wide to feed, too heavy for the decoiler, wound on the wrong core or supplied with edge quality that fails the next forming step.
Here “titanium coil” means a continuous flat-rolled sheet or strip. A titanium tube bent into a coil is a different product with an OD, wall, bend radius and pressure/flow questions; this guide does not specify one.
The short answer: Confirm that you need flat-rolled material, then provide grade and standard, thickness × width, condition, tolerances, edge and surface, coil ID/OD and weight limits, winding direction, join policy and inspection requirements.
1. Is the requirement actually for flat-rolled coil?
In purchasing conversations “titanium coil” can refer to flat strip, a tube formed into a heat-exchanger coil or even a wound wire package. Those are different cross-sections and standards. If the requirement is tube, provide outside diameter, wall, coil diameter and service data to the tube and pipe team. This page concerns only continuous flat-rolled titanium sheet and strip.
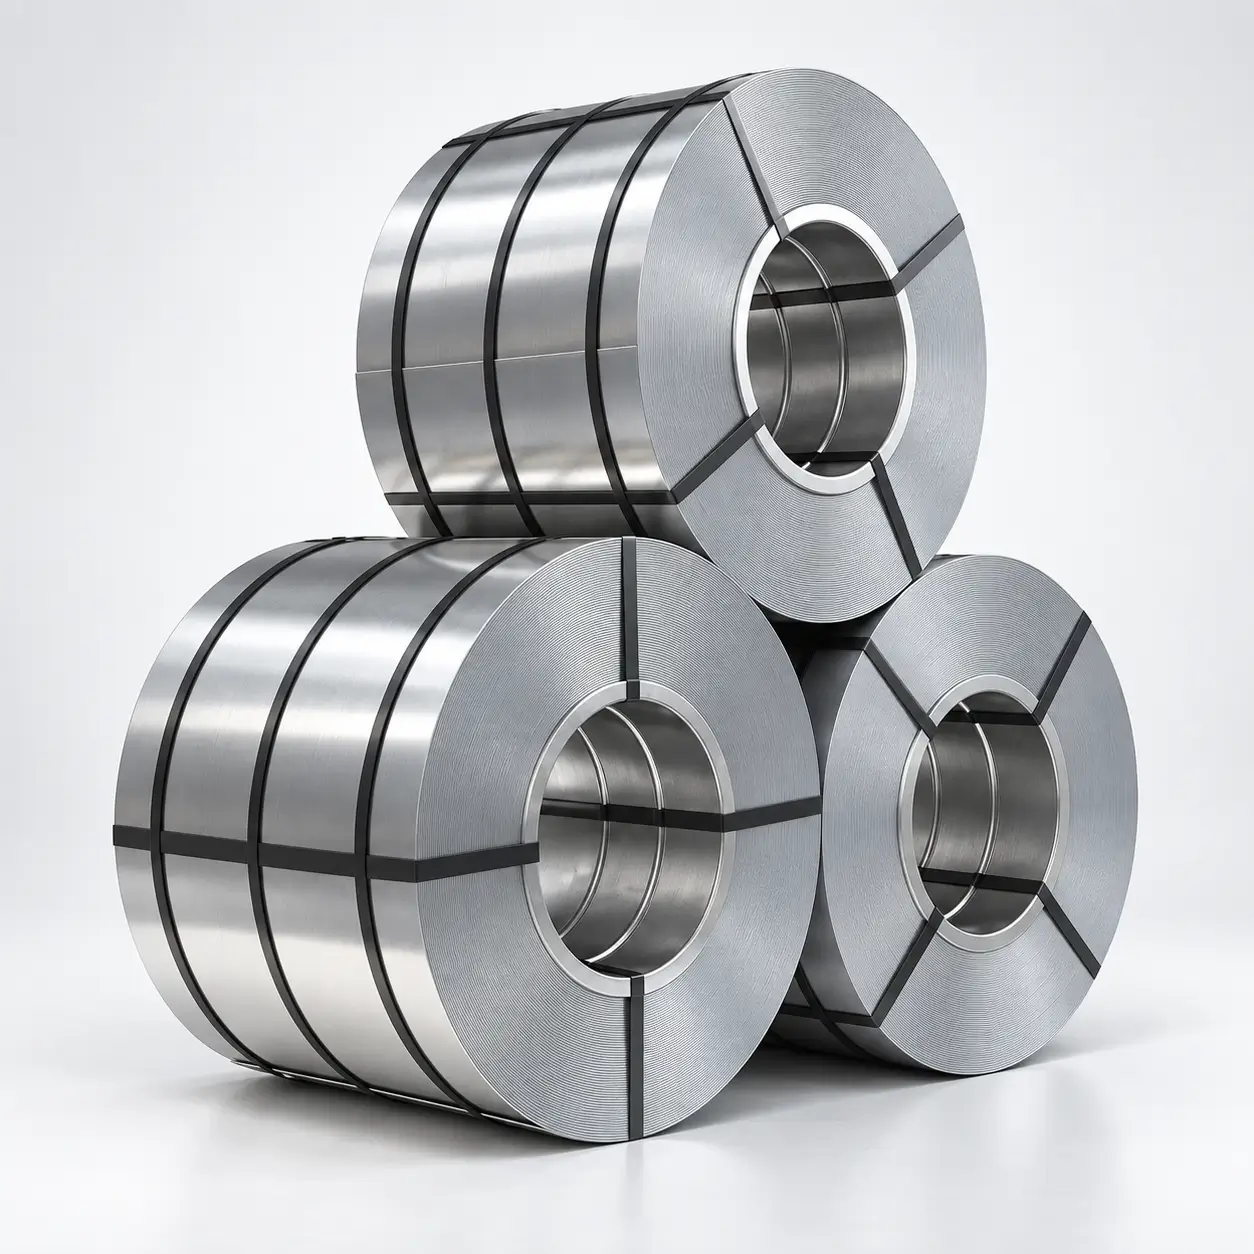
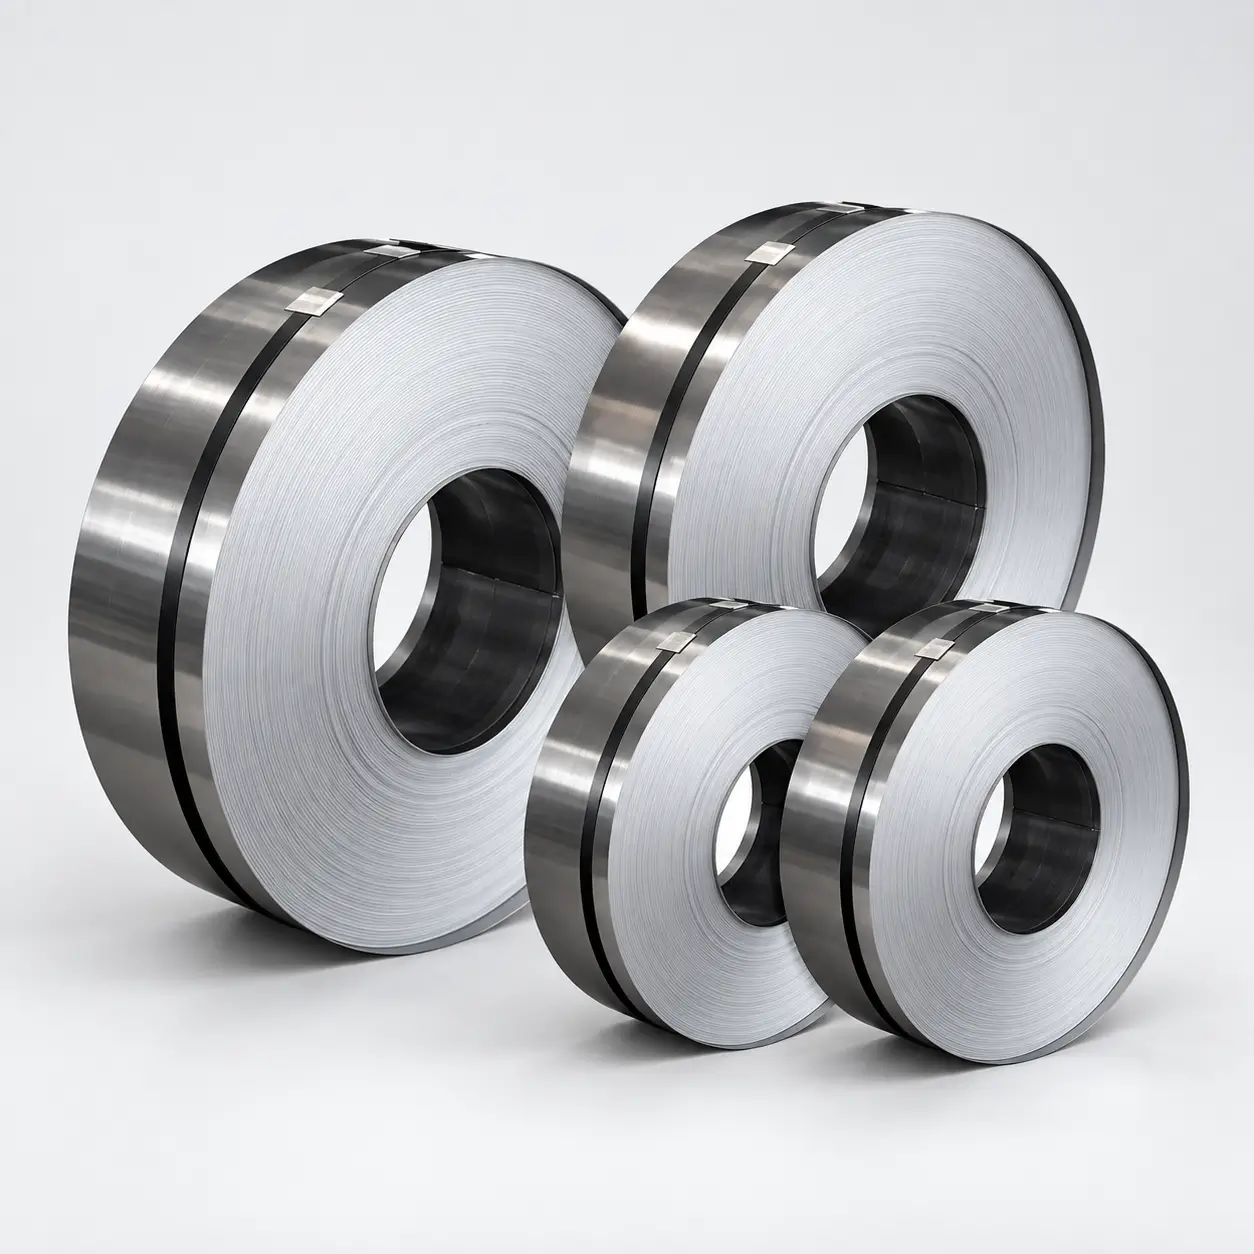
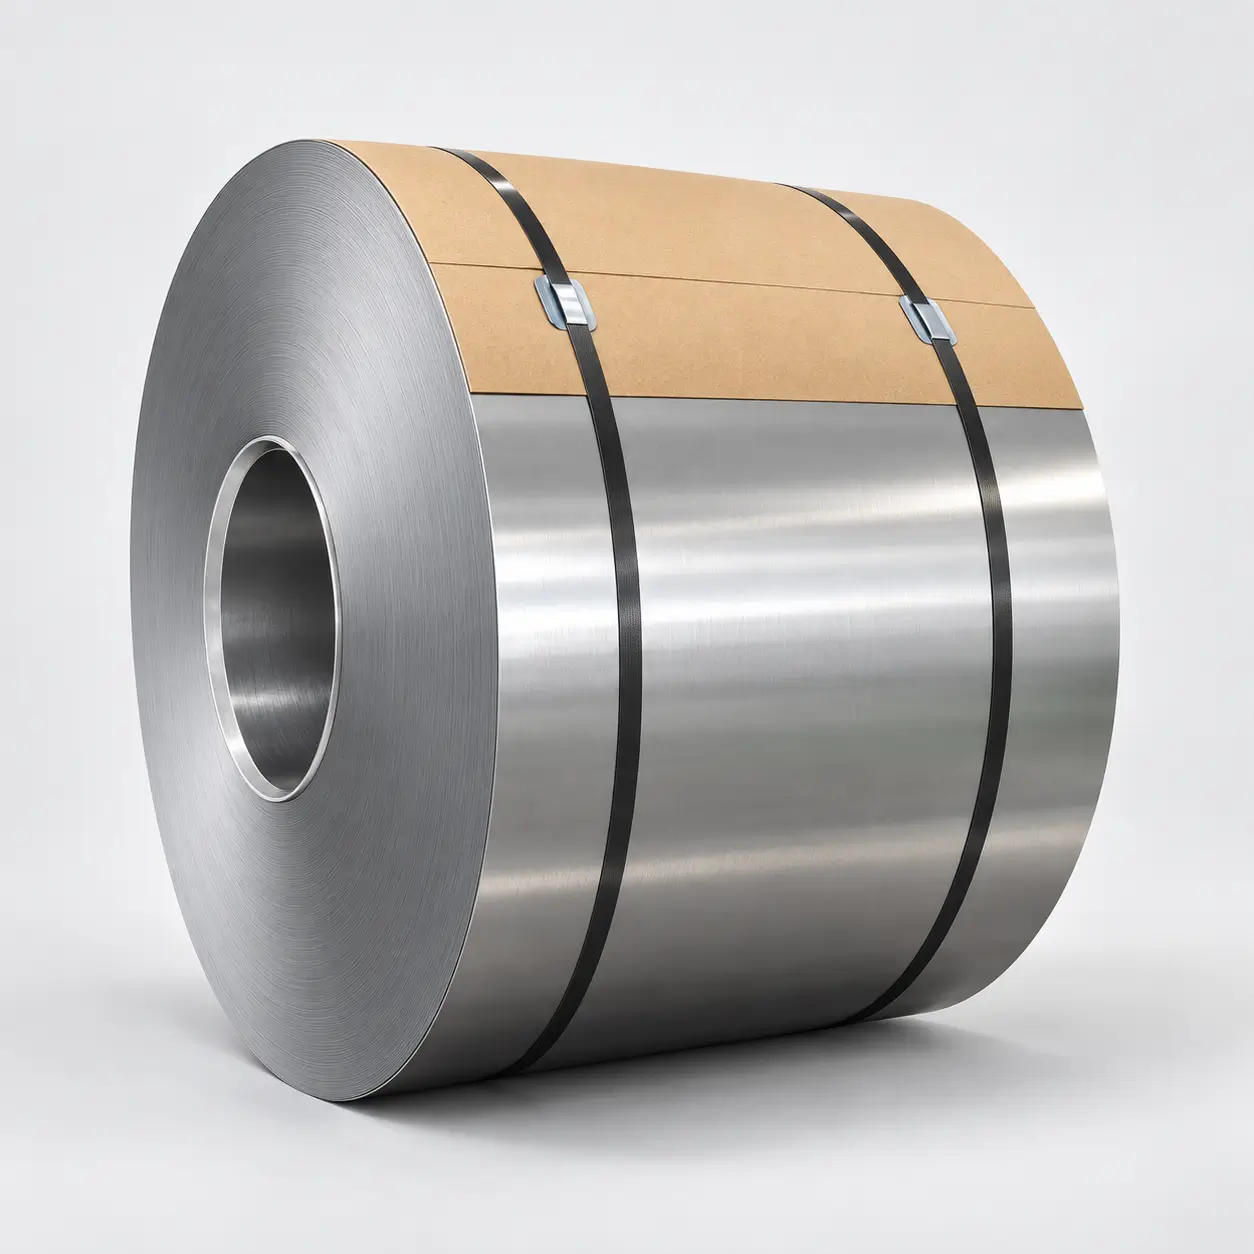
The next distinction is the item delivered. A master coil is wider parent material. A slit child coil has been converted to the width your line uses. Cut-to-length sheets may originate from coil but arrive as a different handling product. A blanket quote for “coil” can conceal the cost and responsibility for slitting, leveling, edge trimming and repacking.
| Delivered form | What the buyer receives | Main commercial question |
|---|---|---|
| Master coil | Parent width for in-house slitting or forming. | Who owns slitting yield and offcuts? |
| Slit strip coil | Narrower child coil ready for a specified feed width. | Are width, burr, camber, core and winding included? |
| Cut-to-length sheet | Sheets converted from coil. | Are leveling, flatness and protective packing included? |
| Thin-gauge coil | Continuous thin stock with heightened handling sensitivity. | Can the required gauge and width be supplied together? |
Choose the route around the next operation. A plant with its own slitter may value master-coil flexibility. A plant with a dedicated press feed may prefer narrower, labeled child coils that load directly. Neither is cheaper in every case once material yield, setup and quality control are included.
2. What changes between master coil and slit strip?
Slitting is not merely a width change. It creates new edges, new child-roll identities and often a new packing plan. Width tolerance, burr height, edge wave and camber may become critical for a guided line. If the parent coil is marked by heat, each child coil must remain linked to that heat through the conversion and shipping documents.
For a repeat job, tell HELE whether you prefer a source-width strategy or a delivered-width strategy. If you specify only the final strip width, suppliers may choose different parent widths and yields. Their prices can differ for reasons unrelated to metal quality. Where offcuts are commercially important, agree whether they are returned, credited or retained.
3. Which grade, standard and condition control the coil?
ASTM B265 addresses titanium and titanium-alloy strip, sheet and plate in its stated scope. ISO 7209:2023 is another flat-product technical-delivery route. A coil order needs the project-selected standard and edition, grade, condition and any extra requirements. The supplier should not apply several standards to every grade and size merely because they appear on a product page.
Condition affects forming, springback and the amount of further processing required. The right grade and condition depend on the finished part or process environment; “stronger” is not a universal improvement. If corrosion service is involved, provide the medium, temperature and exposure. If the coil becomes welded tube or a formed component, that downstream product has additional requirements beyond the flat-stock certificate.
Do not infer actual HELE availability from a broad thickness range printed on an older page. The feasible combination is grade + condition + thickness + width + tolerance + coil mass. An offer should confirm that combination in writing. This is especially important at very thin gauges or uncommon widths, where a short sample may not represent the intended production roll.
4. Will the roll fit and feed through the equipment?
Coil ID is the interface to the mandrel. Maximum OD and unit weight are handling limits. Winding direction, eye orientation and the location of the leading end can determine whether the material enters a line without rewinding. These details can be cheap to define and expensive to correct after delivery.
- Core and envelope: required coil ID, maximum OD, unit weight and allowable width.
- Payoff: winding direction, eye orientation, leading-end accessibility and whether a tail must be secured.
- Continuity: minimum uninterrupted length and whether welds, splices or multiple pieces on one core are allowed.
- Equipment limits: any tension, flattening or straightening constraints that would damage the material.
- Packing: orientation, cradle/pallet design and protection from shifting and edge contact in transit.
A coil may meet its mill dimensions but still telescope or acquire edge dents during transport. If the line cannot run a dented edge, agree edge protection and receiving checks as part of the purchase. For cut-to-length sheets, the relevant handling questions change to flatness, interleaving and stack protection.
Qualify production delivery, not only a small sample
A short strip can test forming or welding response, but not a full roll’s winding or continuous feed. If the first order is a trial, specify which properties it will qualify and which still need confirmation at production scale. A trial under one grade and width cannot validate a different grade-width-gauge combination without review.
5. Which edge, shape and surface details matter?
Different downstream processes see different defects. A press feed may be sensitive to edge burr and camber. A welded-tube line may be sensitive to width consistency and surface contamination near the weld. A flat component may care about coil set or waviness after leveling. “Premium finish” is less useful than naming the defect that causes rejection and the method used to check it.
| Feature | Why it may matter | Define how it is checked |
|---|---|---|
| Gauge and width | Part geometry, tooling fit and process consistency. | Sampling positions along length and across width. |
| Burr and edge wave | Tool wear, feeding, joining and operator handling. | Edge condition, direction and acceptance limit. |
| Camber and coil set | Tracking and final flatness. | Measurement span and state after unwinding/leveling. |
| Surface condition | Forming, bonding, welding or appearance. | Allowed marks, cleaning state and packing protection. |
Never treat a measurement without its state as a universal result. Flatness measured on a tensioned line is not the same as free-sheet flatness. Width near a slit edge may differ from a sample taken elsewhere. For a critical process, agree the sampling plan and reporting format before production.
Decide how local defects affect usable length
In some lines, a marked local surface defect can be cut out without losing the rest of the roll. In others, stopping the line or making a splice is unacceptable. The RFQ should say whether the supplier may mark nonconforming segments, whether they count toward invoiced length and whether a roll can contain more than one piece. This decision changes both inspection and price. It also prevents a shipment from being accepted by total weight while providing less continuous material than the machine needs.
A roll map can be useful for high-value orders: it identifies child-coil ID, nominal length, joins and agreed exceptions. It is not needed for every routine order. Choose the record because it supports the line’s receiving and production decision, not because it makes the certificate pack thicker.
6. What evidence makes coil offers comparable?
A material certificate connects the grade and specification to the parent heat or lot. A slitting record connects that parent material to each delivered child coil. Dimensional inspection establishes the agreed gauge, width and edge characteristics. Packing labels then let the buyer receive each coil without losing that chain. A certificate for the parent material is not a dimensional report for the converted strip.
Ask suppliers to quote the same delivered form and report set. One may include slitting, edge checks and protected reels; another may quote only a mill coil. Compare cost per accepted, usable length or area when the line consumes material that way. Price per kilogram can hide edge scrap, conversion work and downtime caused by a roll that does not fit.
MOQ and lead time depend on source availability, grade, thickness-width combination, conversion, inspection and quantity. Ask whether the quoted stock is identified now or will be sourced after order approval, and from which milestone the lead-time clock starts.
7. What should a coil RFQ include?
- Confirm flat-rolled coil/strip rather than tube coil or wire.
- Application, grade, material specification/edition and condition.
- Thickness × width, tolerances, parent or child-coil form, quantity and annual demand.
- Edge, surface, shape and continuity requirements with acceptance method where critical.
- Coil ID, maximum OD and mass, winding/eye orientation, core and packing constraints.
- Material certificate, slitting traceability, dimensional report and delivery location.
HELE’s titanium coil product page identifies the flat-rolled product family. A useful quotation should turn the buyer’s line interface and material requirement into a confirmed delivered-coil configuration, not simply repeat a catalog thickness range.
Questions buyers often ask
Does titanium coil mean tubing bent into a coil?
Not in this guide. It means flat-rolled sheet or strip. Tube coil requires OD, wall, bend and fluid-service information.
Does ASTM B265 prove a slit coil will feed properly?
No. It addresses applicable flat-product material requirements. Child-coil width, burr, camber, winding and machine fit need separate order controls.
Can a sample strip validate full production coils?
It can validate only the properties and conditions represented by that sample. Production-width, coil mass, winding and continuous feed may need separate confirmation.