A foil quote that names only thickness leaves out half the engineering problem. The same nominal gauge may be available as a narrow strip but difficult to supply at the width, flatness, surface and continuous length your process needs.
Very thin stock can wrinkle, scratch, telescope on a coil or pick up edge damage during slitting and handling. A certificate confirming the metal grade will not tell you whether a particular roll feeds, forms or cuts the way your equipment requires.
The short answer: Specify the end use, exact grade and applicable flat-product standard, then give thickness and width together, acceptable variation, condition, surface, roll or cut-sheet form, inspection method and protective packing.
1. Are you buying foil, slit strip or small sheets?
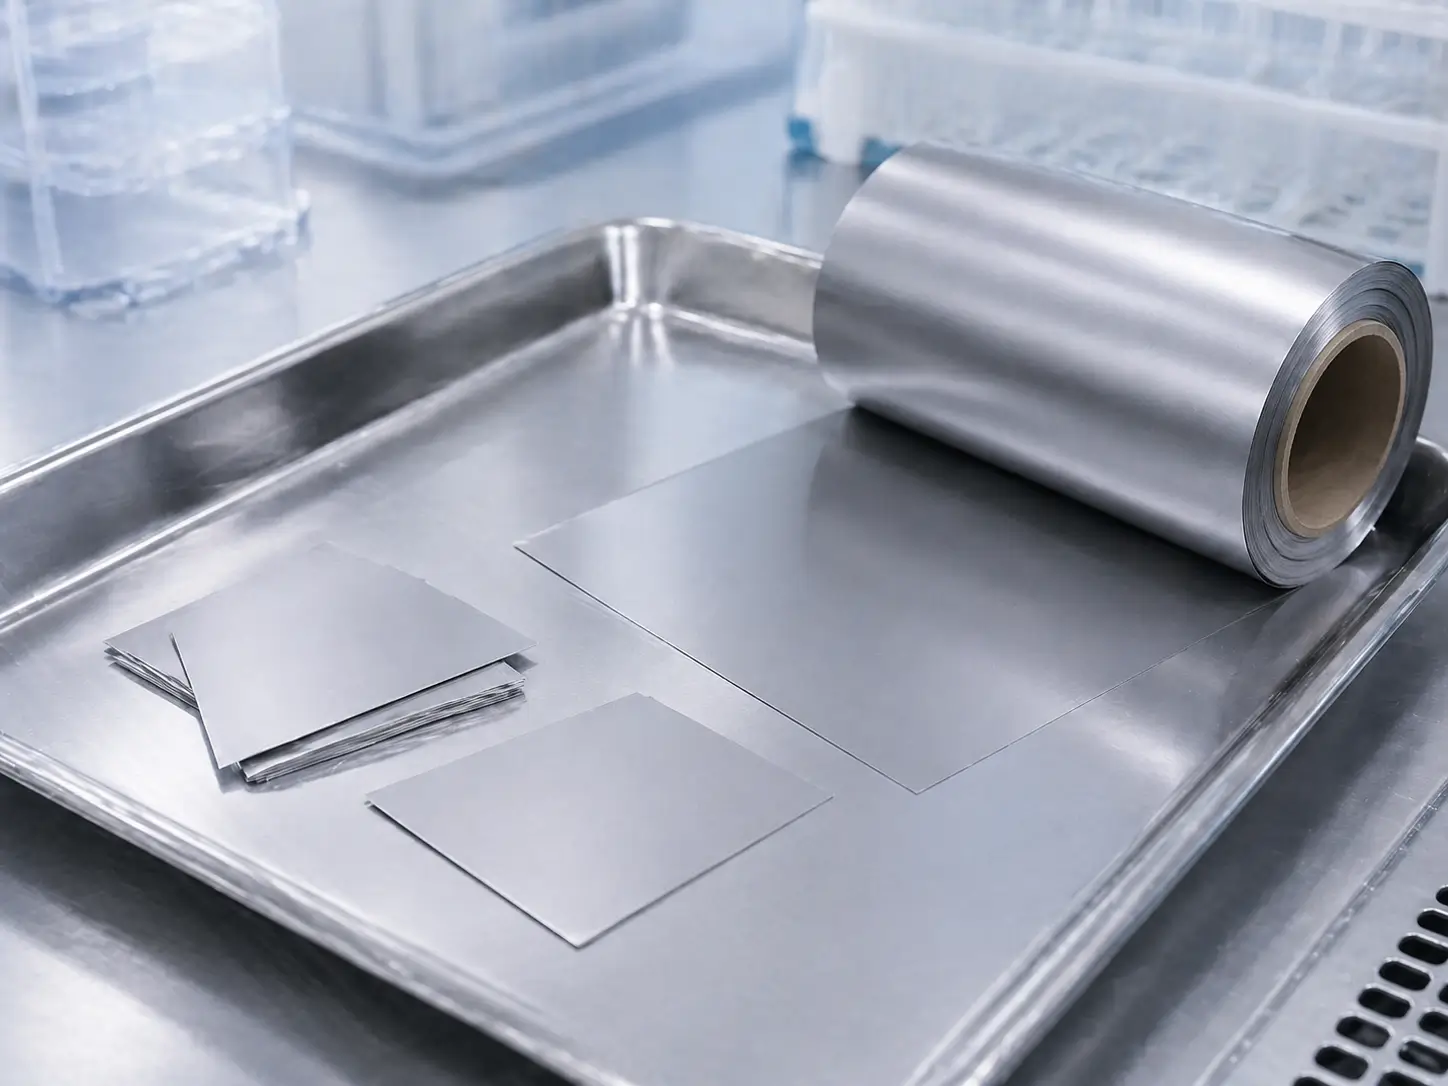
“Foil” is a useful commercial description for thin material, but it does not automatically define a separate ASTM product specification, a standard coil size or a finished-part tolerance. The buyer may need full-width coil, slit strip, cut sheets or shaped blanks. Those forms call for different width control, edge condition, packing and handling.
| Delivered form | Useful when | Check before comparing prices |
|---|---|---|
| Full coil | Your line can process a continuous web. | Coil ID/OD, net weight, maximum joints, winding and usable length. |
| Slit strip | Your process needs a narrower feed width. | Edge burr, camber, width variation and identification after slitting. |
| Cut sheets | Manual or batch processing is more practical. | Flatness, corner and edge protection, interleaving and sheet count. |
| Cut blank | A defined downstream envelope saves handling. | Cutting allowance versus the final part and who owns yield loss. |
State where supply ends. A flat sheet that will later be stamped is not a formed component. A slit strip with a clean material certificate is not necessarily free of edge burrs or camber. If your process cannot accept joins, require a minimum uninterrupted length rather than only a total coil mass.
Start with the processing equipment
A roll-to-roll line needs different information from a workshop cutting individual sheets. Share the feed width, permitted coil dimensions, tension or winding constraints, and whether a protective interleaf is usable. For stamping, the blank layout and rolling direction may matter more than coil OD. The aim is to buy material that reaches the process in a useful state, not merely material that meets a chemistry line.
2. Which grade and material specification apply?
ASTM B265 covers titanium and titanium-alloy strip, sheet and plate in its stated conditions. ISO 7209:2023 is another technical-delivery route for plate, sheet and strip. If a project calls its thin stock “foil,” the purchase order still needs to identify the applicable material specification and edition, grade, condition and additional foil-specific requirements. Do not assume the word foil alone establishes them.
Grade 1 and Grade 2 can behave differently in forming and have different material requirements. An alloy grade such as Grade 5 is not a general substitute for commercially pure titanium merely because stronger material sounds preferable. Decide by the drawing and process: forming strain, corrosion medium, joining, strength and any customer qualification. Where the design authority fixed the grade, get written approval before offering an alternative.
When a project names two standards or a customer specification, ask for a heat-specific compliance comparison rather than placing both standard titles on the quote. Standards differ in scope and editions; a general product-family page cannot establish dual compliance for a particular coil.
3. Why must thickness and width be reviewed together?
A supplier’s minimum thickness often applies at a restricted width, alloy, condition or batch size. As width grows, maintaining gauge, flatness and handling integrity can become more demanding. That is why an isolated “minimum foil thickness” or “±1 μm tolerance” is not a meaningful company-wide promise. Request the exact thickness–width–quantity combination and the inspection method that will support it.
- Thickness: nominal value, permissible range, measurement method and sampling positions across width and length.
- Width: delivered width, edge tolerance and whether the strip will be slit after rolling.
- Length: minimum continuous length for coil supply, or length and sheet count for cut pieces.
- Flatness and shape: whether waviness, curl or telescoping will prevent feeding or downstream assembly.
- Edge: whether slit burr, edge wave or sharp corners create a handling or forming problem.
Consider two offers for the same nominal thickness. One provides a narrow slit strip with acceptable edge quality; the other offers a much wider coil but leaves gauge uniformity and slitting outside scope. The lower price per kilogram cannot tell you which one your line will actually use. Compare the yield and usable area after slitting, cutting and rejecting damaged edges.
Define the inspection state
Foil can change shape when it is uncoiled, cut or laid flat. A flatness claim on a tightly wound coil is different from a measurement on a free sheet. If flatness matters, specify whether the sample is supported, tensioned or free, and at which stage it is checked. The same principle applies to thickness readings near a slit edge or after a forming operation. Agree the state first, then the number.
4. What condition and surface does the application need?
Annealed and cold-worked conditions may have very different forming behavior. Surface appearance alone cannot identify condition or strength. Name the condition required by the applicable standard and your process, and use a material record or agreed test to verify it. If forming, welding or coating follows, tell the supplier which operation is sensitive to surface residue or damage.
“Bright,” “pinhole-free” and “clean” are not complete acceptance terms. A pinhole requirement needs an inspection method, inspected area and rejection threshold. A cleanliness requirement needs a contaminant or residue limit and a way to measure it. Cosmetic surface quality may be sufficient for one use but irrelevant to another that will etch or coat the foil. Order the checks that protect a real downstream process.
For foils used as trial substrates in electrochemical work, do not assume a good raw-material certificate predicts coating adhesion or cell performance. Pretreatment, coating chemistry, current distribution and process validation remain separate. A buyer can ask for material traceability and surface condition at the supply boundary, then qualify the coated component in the actual process.
5. How do you inspect and protect thin stock?
Thin material can arrive damaged even when it left production within tolerance. Excessive winding tension, loose coils, rough contact surfaces and poor edge protection can create creases, scratches or telescoping. Packing is therefore part of usability, not a decorative add-on. Specify core size, orientation, interleaf or protective film if compatible, moisture protection and a limit on package mass that the receiving team can handle.
| Evidence or protection | Decision it supports | Specify in the order |
|---|---|---|
| Material certificate | Is this the ordered grade and lot? | Heat/lot link, standard edition and document type. |
| Gauge/width report | Will the material fit the process window? | Method, measurement positions and sample plan. |
| Surface or pinhole check | Can visible or through-thickness flaws disrupt the process? | Definition, inspected area and acceptance level where needed. |
| Coil or sheet packing | Will the material arrive usable? | Core, winding, interleaving, edge and handling protection. |
Identification must survive slitting and repacking. A certificate for a parent coil has limited value if each narrower delivered roll cannot be linked back to it. At receipt, verify labels, package condition and sample dimensions before removing the foil from its protective environment. If a damaged package is opened and mixed with other rolls, a later claim becomes harder to investigate.
6. Why do foil quotations differ?
Grade and source matter, but yield may dominate. A thin, narrow strip may require slitting from a wider parent coil; a wide, very thin product may need a different production route. Surface treatment, inspection, cut-sheet conversion and special packing add scope. Minimum order and lead time depend on the exact combination rather than on the generic label “titanium foil.”
Compare price per usable area or accepted roll where that is how the buyer consumes material. Ask whether quoted mass includes edge trim or whether the price is for the net delivered strip. If a supplier proposes a wider coil for you to slit, include your own slitting yield and labor. If you need prototypes before regular supply, say which parameters the prototype must represent; an unusually narrow sample may not validate a wider production width.
Practical comparison: hold grade, thickness, width, condition, surface, inspection, package and minimum continuous length constant before comparing unit prices.
7. What should the RFQ include?
- Application and next processing step: roll-to-roll, stamping, cutting, forming, coating or another use.
- Grade, governing flat-product or project specification and edition, and required condition.
- Thickness × width, tolerances, quantity, roll/sheet form and minimum continuous length if relevant.
- Surface, pinhole, flatness, edge and cleanliness criteria with methods where the process requires them.
- Core and package limits, material traceability, inspection reports and delivery location.
Share a sample drawing or equipment interface when possible. HELE’s titanium foil product range is the right entry point for a specific grade and format review; an order-specific offer should identify the available thickness–width combination and the included evidence.
Questions buyers often ask
Does ASTM B265 have a separate category called foil?
Its published title covers titanium strip, sheet and plate. An order using “foil” should still name the applicable material specification and add the required thin-stock dimensions and acceptance criteria.
Can a supplier guarantee “pinhole-free” foil from a product photo?
No. Define how much area will be inspected, by what method, and what constitutes a rejectable hole or flaw.
Is the thinnest sample a reliable production specification?
Only if the intended production width, grade, condition, tolerance, package and quantity are also demonstrated or confirmed.