An elbow can arrive in the correct titanium grade and still hold up installation because its outside diameter, wall or weld-end preparation does not match the pipe on site.
“Titanium pipe fitting” is a family, not one commodity. A butt-weld elbow, socket-weld coupling and lap-joint stub end are made and inspected differently. A supplier can only quote comparably when the buyer identifies the delivered fitting and the line interface.
The short answer: Provide the line drawing or isometric, fitting type and construction, grade and applicable product standard, pipe OD and wall/schedule, end preparation, service conditions, NDE/test requirements and the exact delivered scope.
1. Which fitting does the line need?
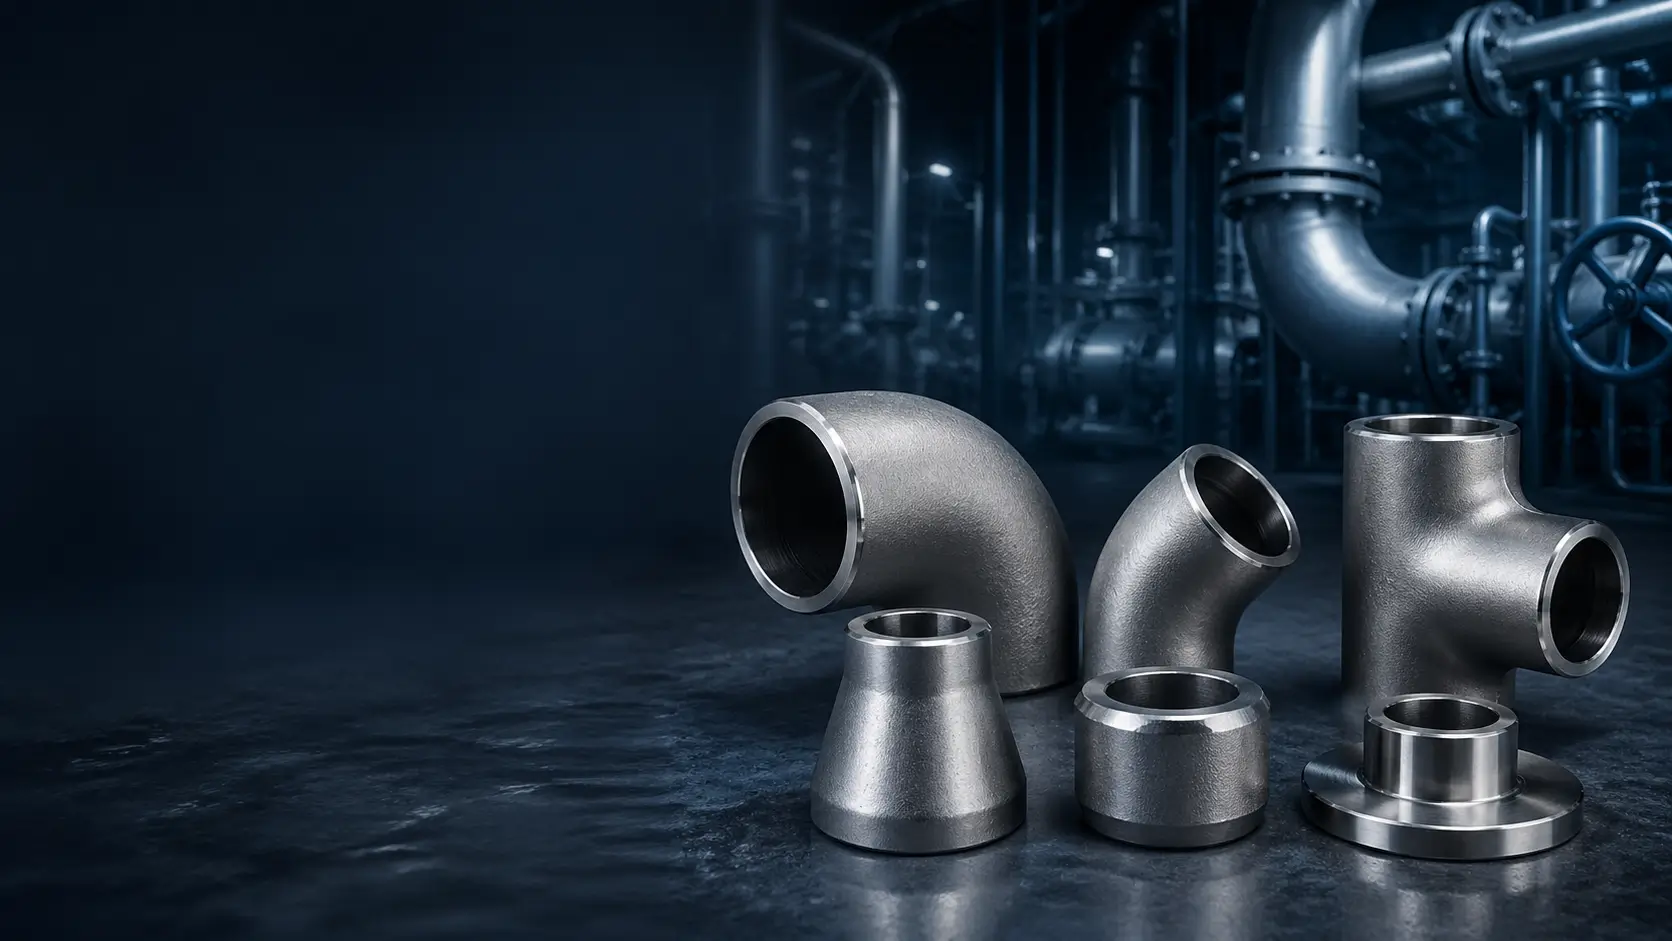
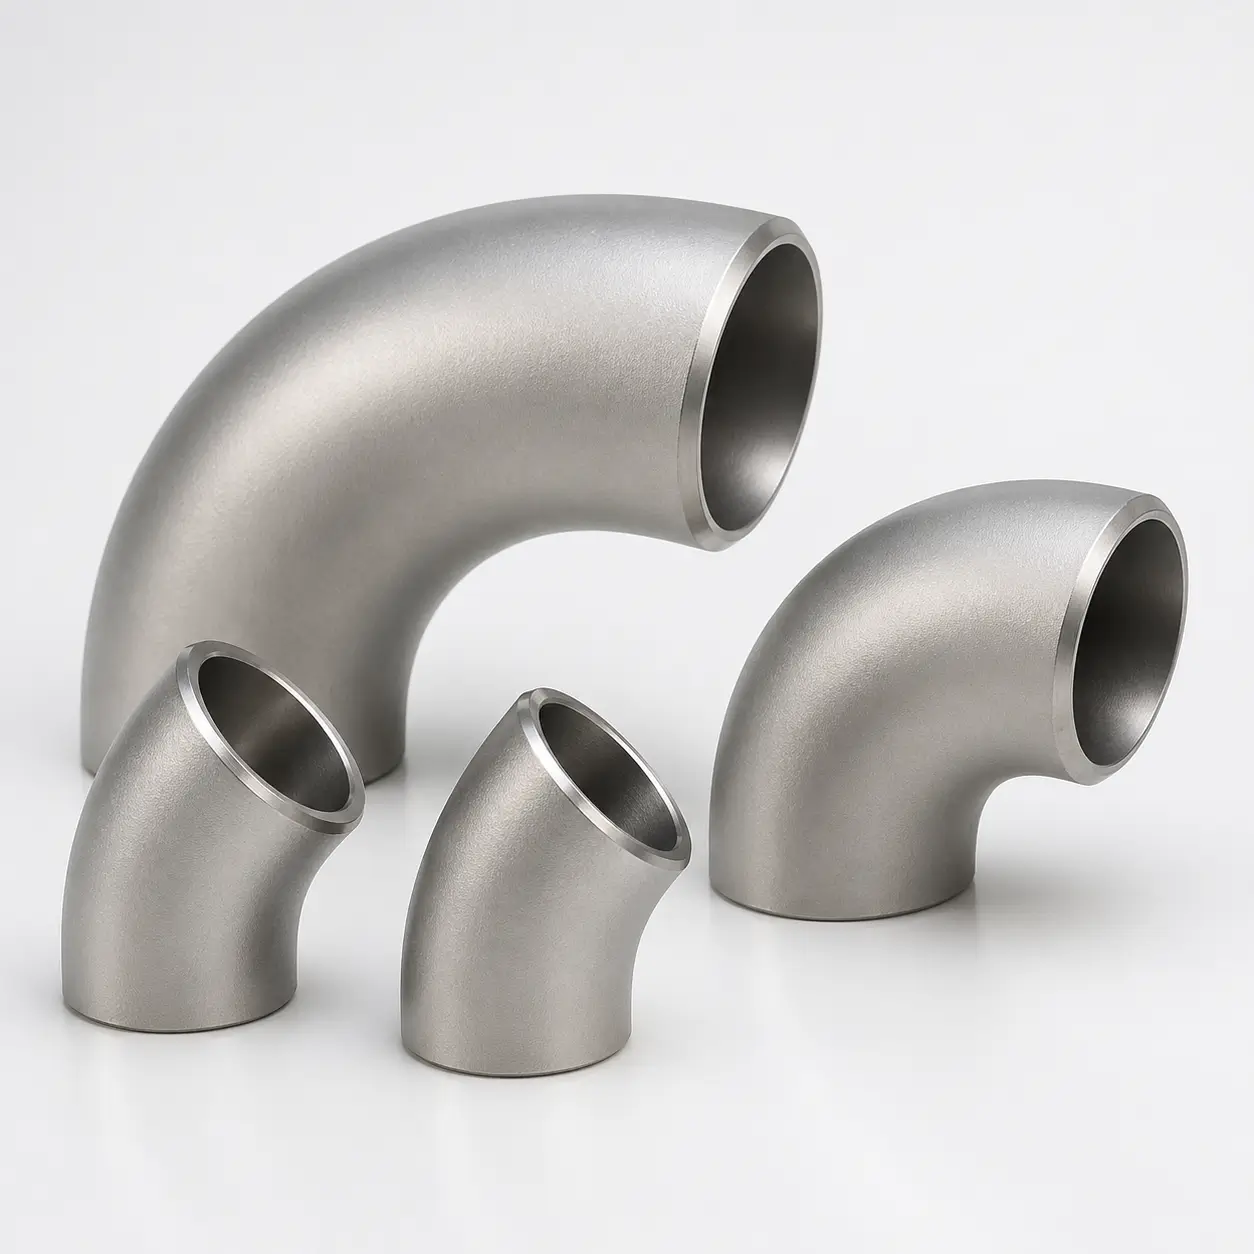
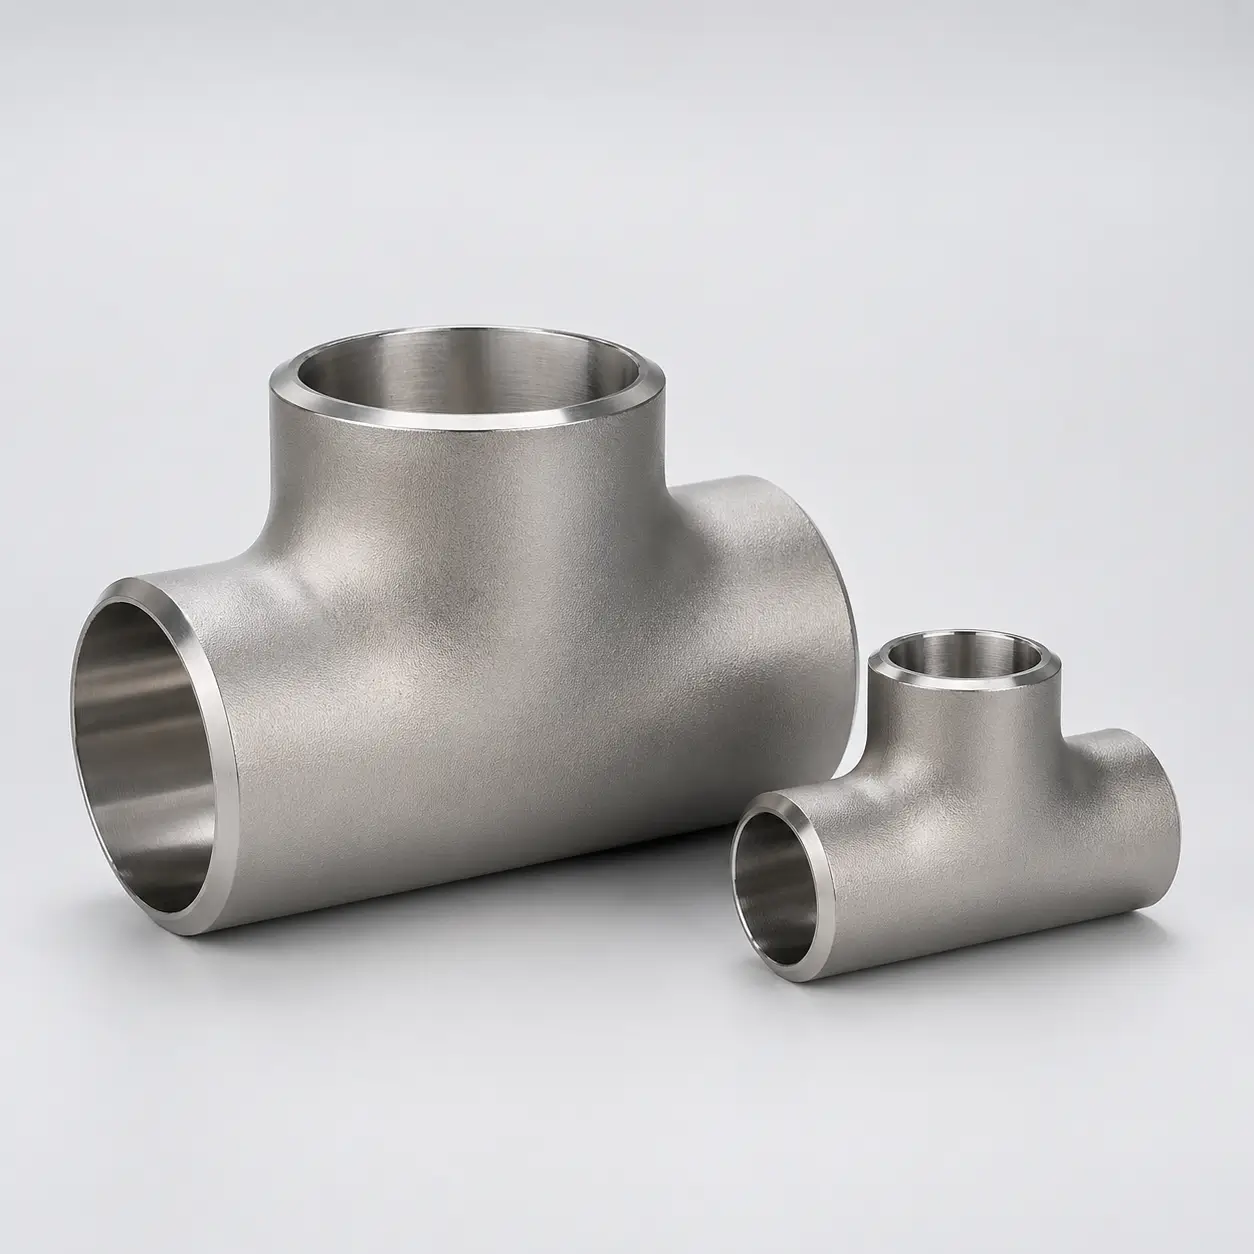
Elbows change direction; tees add a branch; reducers change size; caps close a line; stub ends support a lap-joint connection. A bend made from pipe and a manufactured elbow can solve a similar routing problem but need different space, wall and inspection allowances. Start with the piping layout and specify the fitting’s actual geometry.
| Fitting | Dimension that often gets missed | Service question |
|---|---|---|
| Elbow or return | Center-to-end dimensions and bend radius. | Can the route fit without unwanted stress or a wall-thin zone? |
| Equal or reducing tee | Branch size, location and transition geometry. | Does the branch match flow and reinforcement design? |
| Concentric or eccentric reducer | End sizes, length and orientation. | Will the orientation create a trap or drain problem? |
| Lap-joint stub end | Lap thickness, face and mating backing flange. | Does the entire connection assemble and seal as designed? |
For a replacement, photographs and a nominal callout may miss the center-to-end dimension, eccentric orientation or the field weld allowance. Provide the old drawing or dimensions taken from an undamaged reference when possible. A removed, worn fitting may not faithfully represent the original wall or geometry.
2. Is the fitting butt-weld, socket-weld or threaded?
ASTM B363 covers seamless and welded titanium/titanium-alloy welding fittings within its scope. ASME B16.9 defines dimensions and other requirements for factory-made wrought butt-welding fittings. A dimension standard does not by itself identify the titanium grade, construction or project-specific pressure suitability.
Forged socket-weld and threaded fittings are a different purchase route; ASME B16.11 addresses their form, dimensions and ratings within its scope. Do not describe a threaded coupling as an ASTM B363 butt-weld fitting just because both are titanium and connect pipe.
The piping code, joint design and service conditions determine whether a proposed fitting route is acceptable. A schedule or nominal “class” is not a stand-alone working-pressure guarantee. If the project’s design code calls for a particular material listing or calculation, share it early rather than asking a supplier to infer the requirement from an NPS number.
3. Will the fitting actually match the pipe?
Nominal pipe size is convenient shorthand, but the installation depends on actual outside diameter, wall thickness, inside diameter and end geometry. Provide the pipe standard and the project’s specified schedule or measured wall. If the pipe is nonstandard, send a dimensioned drawing. A fitting made to a familiar nominal size may still require a transition or a special bore to align with the pipe.
- OD and bore: confirm the pipe’s actual dimensions and whether an ID match or specified transition is required.
- Wall: distinguish nominal pipe schedule from the minimum wall needed after forming and at a fabricated branch.
- Ends: define bevel, land, squareness and any weld preparation under the project’s procedure; ASME B16.25 may be relevant where specified.
- Space: show center-to-end, overall length, branch location and reducer orientation.
- Connection: identify whether backing flanges, gaskets, bolts or field-weld consumables are included or excluded.
For an eccentric reducer, mark “flat on top” or “flat on bottom” only after considering the line’s drain and vent purpose. That orientation can be more important to operability than a small unit-price difference between two nominally similar reducers.
Check fit before fabrication begins
Where the piping is already installed, a dimensioned field sketch can prevent rework. Record distances between fixed tie-in points and the tolerances the installation can absorb. Do not try to correct a missing pipe dimension by simply widening a weld gap; the fit-up and welding procedure should be reviewed by the responsible piping team.
4. How do forming and welding affect the delivered item?
Construction changes which surfaces and joints need attention. A formed elbow can have different wall distribution around the bend. A welded fitting adds a weld seam and its associated inspection requirements. A fabricated tee introduces a branch junction whose geometry and reinforcement should be reviewed against the piping design. None of these routes is automatically inferior; they are not automatically interchangeable either.
Titanium welding requires protection from atmospheric contamination while the metal is hot. The project welding procedure, fit-up, cleaning and shielding should be controlled by the fabricator or installer responsible for the joint. A fitting that arrives clean and dimensionally correct can still be damaged by poor field handling or welding. Agree where shop fabrication ends and field work begins.
| Supply boundary | Supplier should clarify | Buyer should confirm |
|---|---|---|
| Bare fitting | Grade, geometry, ends and inspection included. | Pipe match and field welding plan. |
| Fabricated spool | Included pipe lengths, shop welds, test and records. | Tie-in dimensions and design acceptance. |
| Stub-end joint package | Stub end, backing flange, gasket and bolts in or out. | Face/gasket compatibility and installation sequence. |
| Special formed part | Starting material, forming route and acceptance. | Design calculation and allowable substitution. |
If a fitting will be pickled, mechanically finished or otherwise cleaned after fabrication, state the required final condition and allowed residues. “Titanium is corrosion resistant” does not mean oil, iron transfer or handling damage can be ignored in every process.
Consider a replacement tee in an existing line. A supplier might offer a correctly graded, dimensionally standard tee, but the branch may be positioned a few millimeters differently from the plant’s old fabricated spool. If two pipe runs are fixed in place, that small mismatch can force cutting and rewelding elsewhere. A field-fit dimension or a short spool drawing often has more purchasing value than asking for a general statement of “high precision.” The inspection report should cover the dimensions the installer cannot adjust.
Weld preparation also changes the work split. A bare square end may be appropriate when the installing contractor prepares every joint under its own procedure. If the project expects machine-beveled ends, ask for the bevel and land on the supplier drawing and protect them for shipping. Neither approach is inherently superior; the mistake is allowing each bidder to assume a different one.
5. Which records support release and installation?
A material certificate should identify the grade and heat of the stock used. A fitting record should connect that material to the finished item. For welded or otherwise critical construction, the project may require weld records, NDE, pressure/leak testing or positive material identification. Ask for the exact acceptance clauses and test scope, not a generic phrase such as “all tests included.”
Dimensional inspection should concentrate on the interface: end OD and wall, center-to-end geometry, branch position, bore and weld preparation. A certificate for plate or tube feedstock cannot prove those finished fitting dimensions. Likewise, a pressure test on an assembled spool should not be claimed for a bare fitting if the quote excludes it.
Marking and packaging matter for site work. Similar-looking elbows with different wall or grades can be mixed during installation. A practical pack list connects each item number to its size, grade, heat and inspection record. Protect prepared weld ends from dents and contamination in transit.
Where the fitting is intended for a corrosive service, a material grade decision should follow the actual fluid and temperature. General corrosion charts can screen possibilities, but crevices, deposits, cleaning cycles and mixed-metal connections may alter local conditions. Ask the process and materials engineer to approve the grade; ask the supplier to provide the specified grade and traceability. That division keeps a product guide useful without pretending that a sales quotation is a corrosion qualification.
A receiving package is most useful when its labels follow the piping item numbers. An inspector should be able to take one fitting from a crate, find its drawing revision and see which heat and test reports apply. A thick bundle of certificates with no item mapping can slow installation more than a small, well-organized record set.
6. How should fitting quotations be compared?
Compare by installable line item rather than by weight of titanium. One bidder may quote seamless material, another a welded construction; one may include end preparation and NDE, another may exclude them. The lower price may be appropriate, but only if the design permits the route and the buyer knows what work remains.
Lead time and MOQ depend on grade, size, wall, construction, tooling, quantity and test scope. Ask whether material is identified or still to be sourced, and whether the delivery date begins after drawing and test-plan approval. For a project with several fittings, supply the full bill of materials so the supplier can propose a sensible manufacturing and inspection sequence.
7. What should a pipe-fitting RFQ include?
- Piping drawing/isometric, line number, medium, design temperature and pressure basis.
- Item-by-item fitting type, orientation, NPS or actual OD, wall/schedule and quantity.
- Grade, applicable material and dimensional standards/editions, permitted construction route.
- Center-to-end or special dimensions, bore match, weld ends and required final surface.
- Material, weld, dimensional, NDE and pressure-test records as applicable; clear supply boundary.
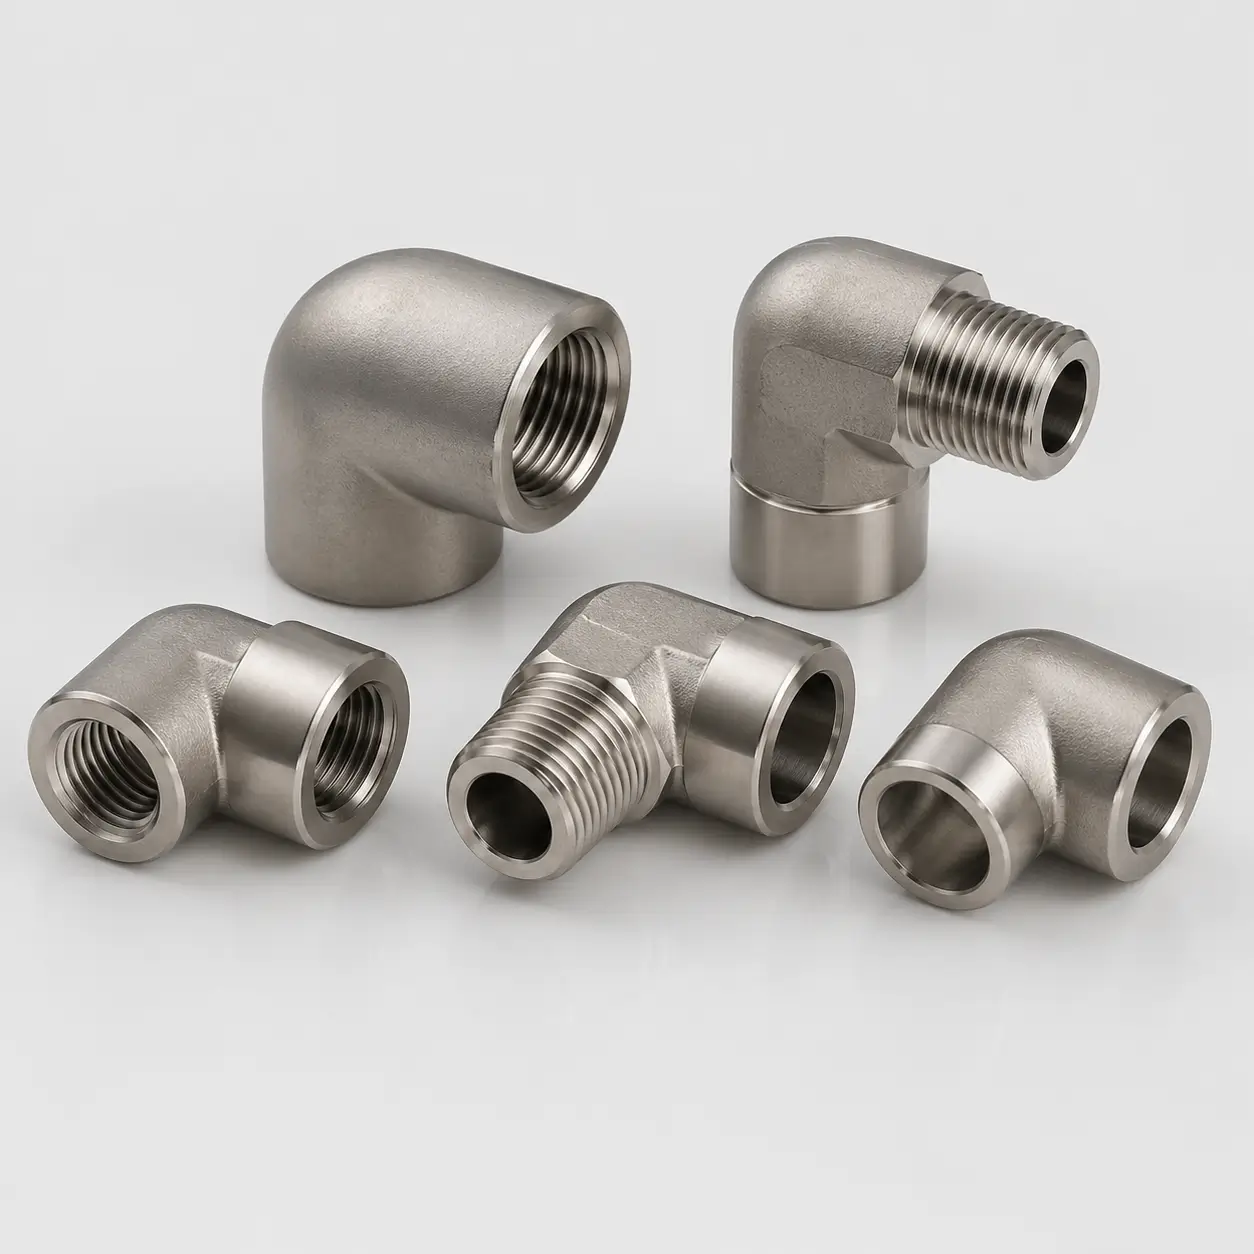
HELE’s titanium fittings product page shows the family. A project quote should turn that broad range into a specific, line-compatible fitting and list exactly which fabrication and acceptance steps are included.
Questions buyers often ask
Does a Schedule 40 titanium fitting have a universal pressure rating?
No. Schedule describes a wall-dimension series, not an all-purpose allowable pressure. The governing piping code, material, temperature, geometry and joint design must be reviewed.
Is ASME B16.9 enough to specify the material?
No. It addresses the butt-weld fitting form and dimensions. The titanium grade, product-material specification and project tests must also be stated.
Can a butt-weld fitting be swapped for a socket-weld fitting?
Not as a silent substitution. The connection design, dimensional standard, size range, welding method and inspection scope differ.