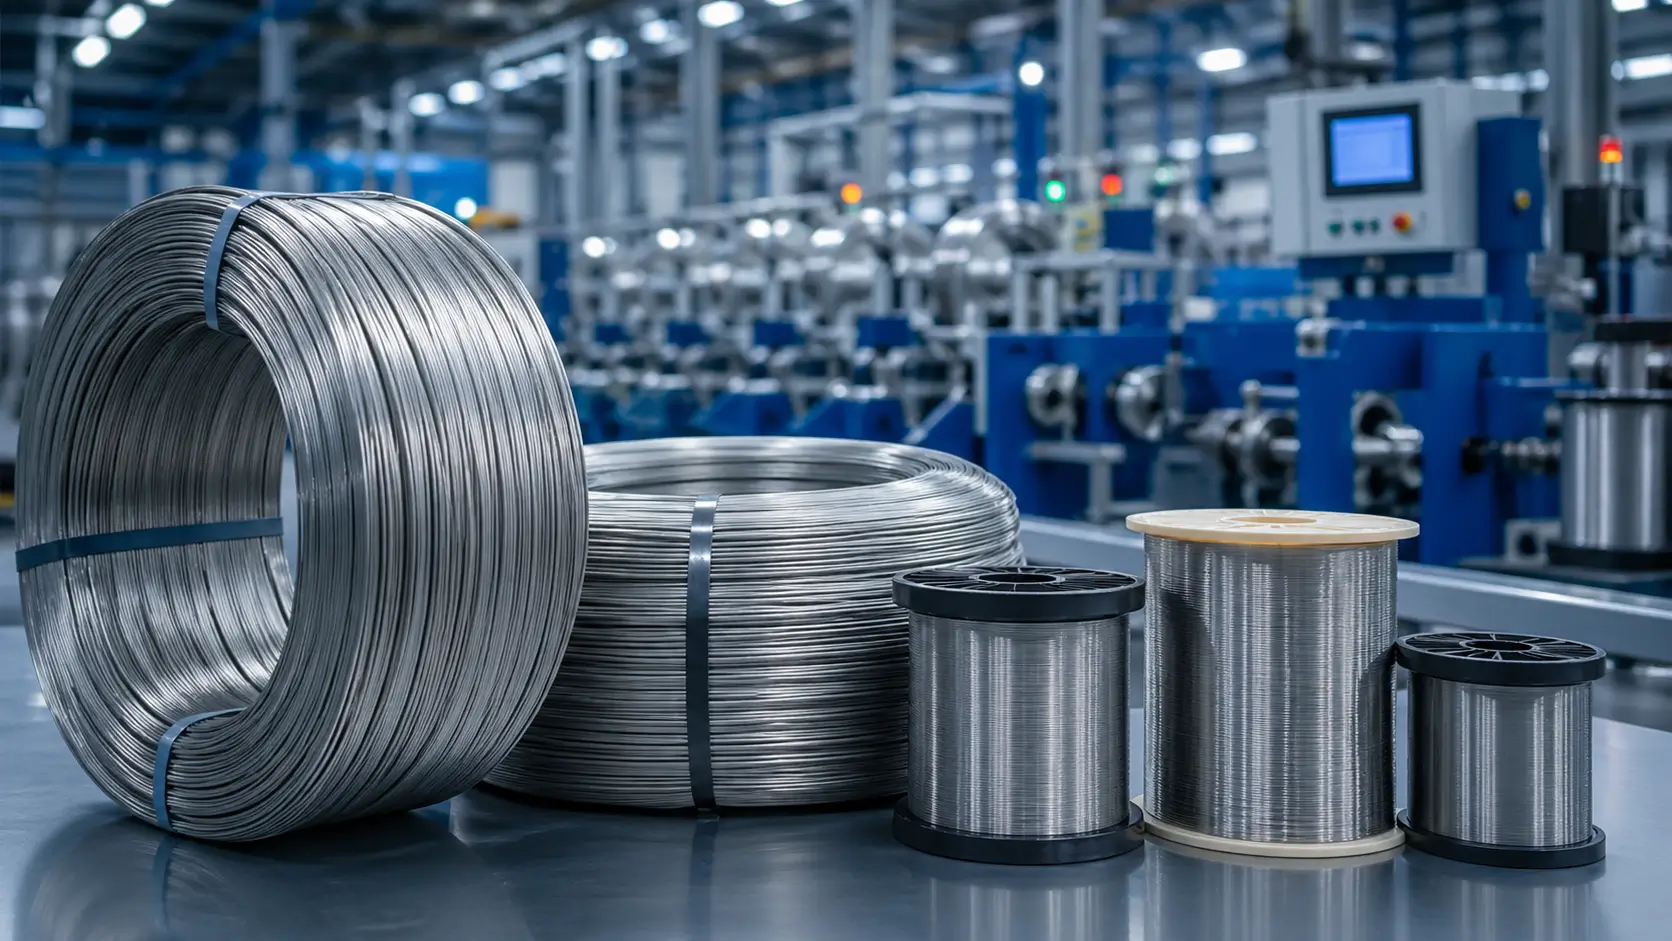
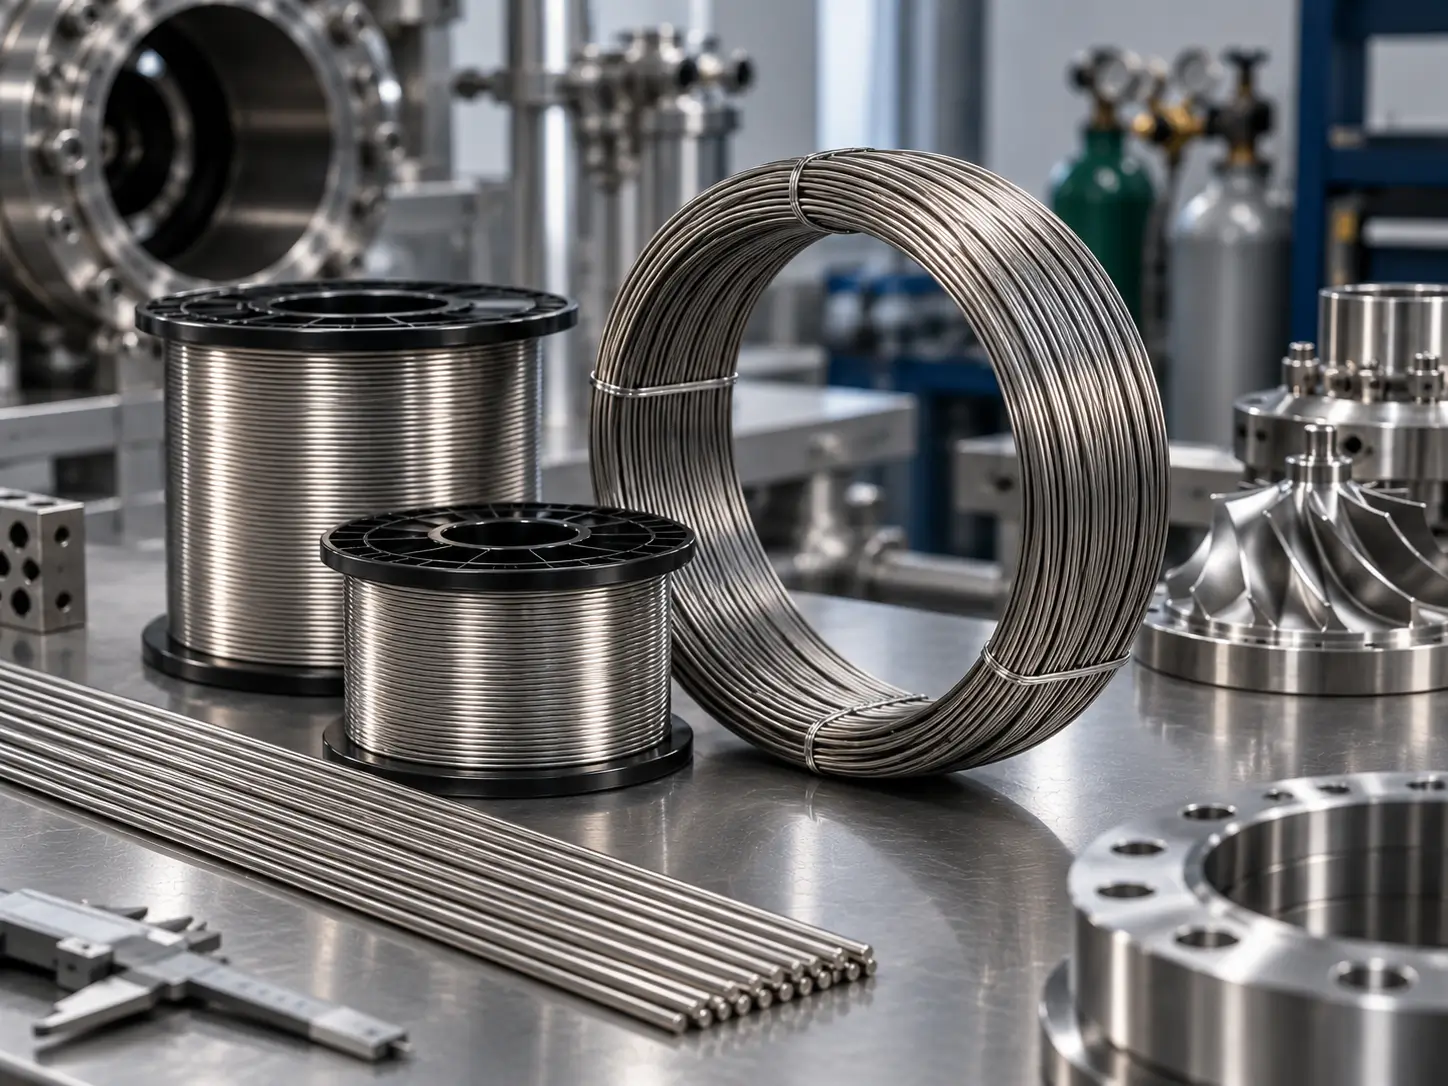
A 1 mm titanium wire can be sold as a coil for forming, a straight length for fabrication or a controlled welding filler. The diameter may be the same, but the useful purchase requirements are not.
A coil can meet its material certificate and still jam in a feeder because the spool, winding or continuous length is wrong. A clean straight rod can look similar to filler metal but lack the specified filler classification. Those are purchasing differences, not cosmetic details.
The short answer: Start with the end use. Then state the governing standard or filler classification, grade, condition, diameter and tolerance, surface condition, package geometry and the lot records you will need.
1. Which wire are you actually buying?
General-purpose wire is normally purchased as material for a later operation: forming, cutting, weaving, fastening or another fabrication step. Welding filler is purchased for a qualified joining process. A precision feeding application may place unusual weight on winding quality, continuous length, cast, helix and cleanliness. Calling all three “titanium wire” hides the decisions that matter.
| Purchase route | What drives the order | Question worth asking |
|---|---|---|
| General wire | Grade, condition, diameter, mechanical properties and delivery form. | Is the wire intended for subsequent forming, machining or electrical use? |
| Welding rod or wire | Filler classification, welding process, diameter, cleanliness and package. | Which procedure and base materials will the filler support? |
| Precision feed wire | Consistent diameter and feed behavior, surface, spool and continuous length. | Which equipment and qualification checks determine acceptance? |
The distinction also changes how to read the quote. A supplier may price wire by net mass, length, number of straight rods or packaged spools. If a line item is based on a different form from the one your process consumes, the apparent unit price is not a meaningful comparison.
Wire, rod and filler are not interchangeable words
“Rod” can mean a solid bar for machining or a straight welding filler rod. The purchase order should resolve the ambiguity with the intended use, standard and delivery dimensions. A short cut piece of general wire does not become an approved welding filler simply because it is straight. Equally, a filler rod classification does not establish that it meets a separate engineering material specification for a finished component.
For a new application, tell the supplier whether you are evaluating a material sample or placing production stock. Trial lengths can reveal winding, cut-end and surface issues before the purchase grows into a full release. The trial should use the same classification and records proposed for production, or the result may not transfer.
2. Which grade and standard control the material?
For general titanium and titanium-alloy wire, ASTM B863 is one relevant product specification. The purchase order still needs the grade, edition if the project controls it, and any supplementary requirements. It is not enough to put “ASTM titanium” in an email and leave the chemistry and condition for a supplier to infer.
For welding electrodes and rods, AWS A5.16/A5.16M is a different route. Its classification addresses filler material; the welding procedure, base metal, shielding and finished weld qualification remain separate project responsibilities. A grade number that sounds familiar is not proof that a general wire heat and a named filler classification are equivalent.
| If the drawing or process asks for… | Put this on the RFQ | Do not assume |
|---|---|---|
| General commercially pure wire | Exact ASTM B863 grade/UNS, condition, diameter and required properties. | All CP grades have the same strength or forming response. |
| Ti-6Al-4V wire | Named alloy grade and the applicable wire specification. | A bar or plate certificate qualifies the wire form. |
| Welding filler | Named AWS classification, process, rod/spool form and package. | A general material MTC replaces filler classification and lot records. |
| Medical or aerospace material | The exact project specification and controlled supply/inspection scope. | A raw-material citation approves the finished device or flight part. |
3. How precise must the diameter and delivery form be?
Diameter is only one part of usability. For a forming die or wire feed, diameter variation along the length may be as important as the nominal size. For short cut lengths, straightness and end quality may dominate. For a spool, the buyer may care about continuous length, winding tension, spool dimensions and whether wire crosses or tangles during payout.
- Size: state diameter, allowable variation and the measurement method or governing tolerance. If the requirement is extremely tight, include the span of wire over which it applies.
- Form: request coil, spool or cut straight lengths explicitly. For spool supply, include flange and hub constraints when the wire enters a machine.
- Length: distinguish minimum continuous length from total supplied length. Spliced or joined lengths should not be presumed acceptable.
- Ends and orientation: for cut rods, define end condition and whether straightness or bend is a receiving criterion.
A published minimum diameter or best-case tolerance from any supplier can apply only to a narrow combination of grade, condition, width of offer and quantity. HELE’s product listing is a starting point; ask for an order-specific, written capability response before designing around an extreme wire size.
Why packaging belongs in the specification
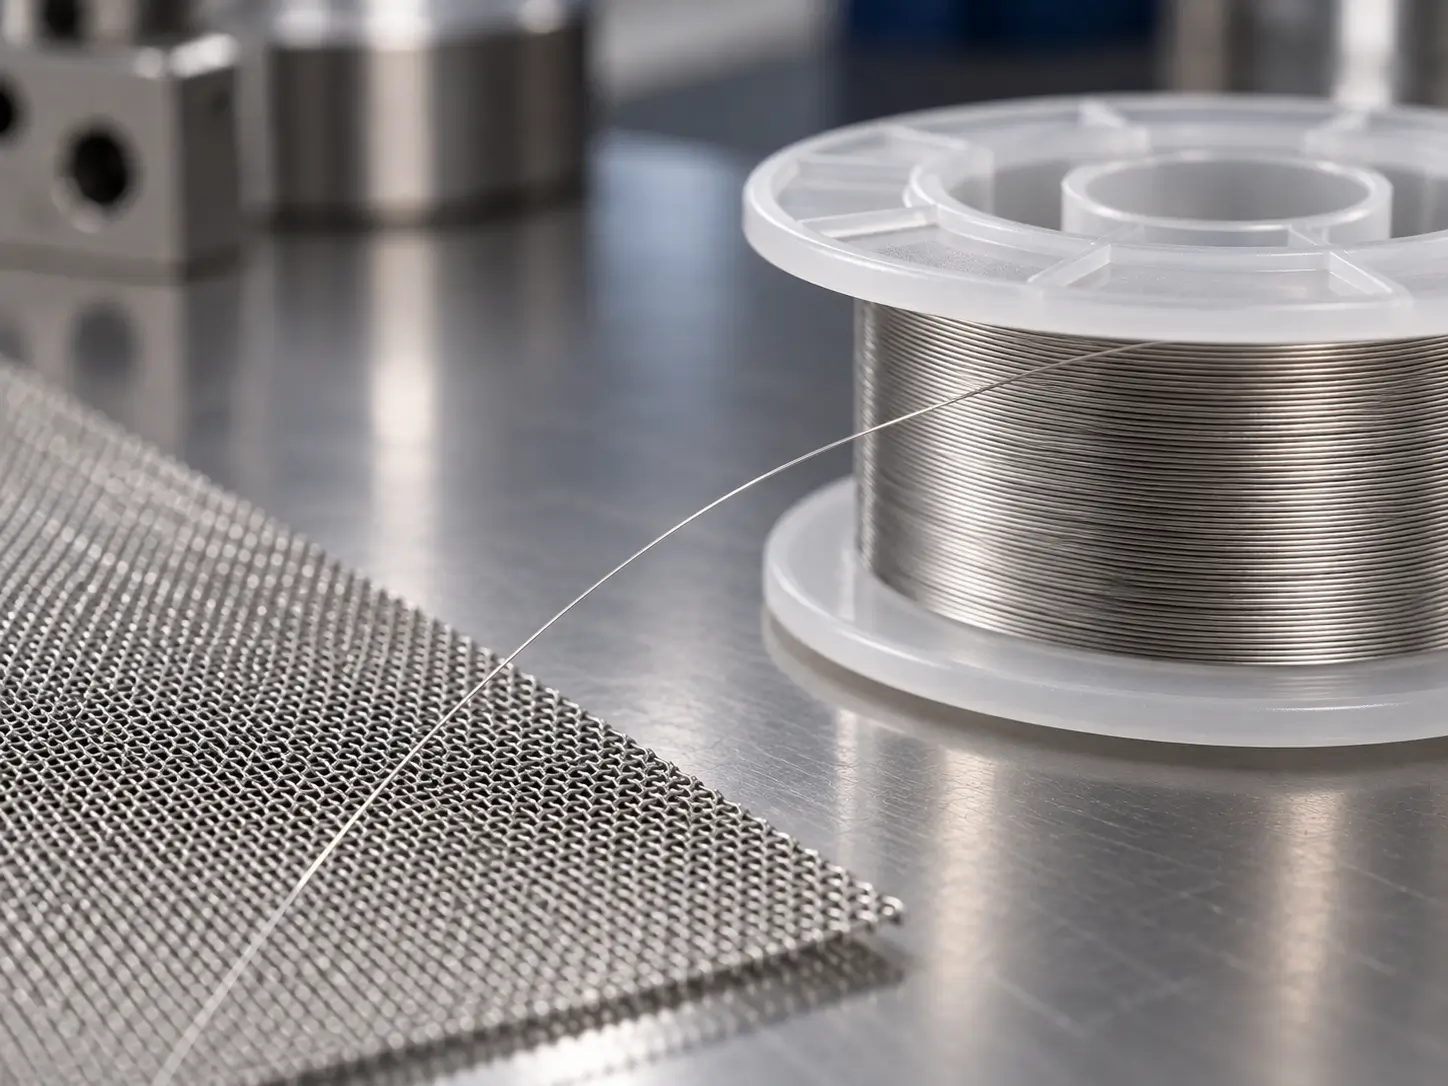
Good wire can be damaged after manufacture. Tight bends, uncontrolled winding and abrasion can create feed interruptions or surface marks. If your process uses a reel directly, provide the reel drawing and target net weight. If you need straight rods, say how they should be bundled and protected against bending in shipment. Price and lead time may change when a long coil must be cut, straightened and packed into protected lengths.
Compare the material the machine can actually consume
Imagine that Supplier A offers a lower price for one large coil and Supplier B offers smaller spools that fit the buyer's feeder. If the large coil has to be rewound locally, the buyer assumes another operation, another handling risk and perhaps another lot-identification step. The cheaper quote may still be right, but only if the buyer has the equipment and accepts that extra work. The same logic applies to short welding rods: buying long stock and cutting it in-house is a different purchase from receiving cleaned, identified, ready-to-use filler rods.
For automated processes, test the proposed package as part of the trial. A short sample of loose wire can confirm chemistry and nominal diameter but cannot demonstrate that a production spool pays off consistently from start to finish. If the final order will use a different spool size or winding process, say so in the trial record and repeat the relevant feed check.
4. What surface condition does the process need?
“Bright” and “clean” sound useful but are not acceptance criteria by themselves. A forming operation may tolerate minor cosmetic marks yet reject scratches that start cracks. Welding filler is sensitive to surface contamination and handling. An electrochemical or medical-material route may have a separate cleaning or processing specification. Describe the process and which marks, residues or coatings would cause trouble.
Specify whether the required state is as-drawn, annealed, pickled, mechanically finished or another agreed condition. Do not assume a treatment is included because it appears on a general product page. Where surface finish or cleanliness matters, define the inspection or test that will prove it and who owns that step.
Surface requests also affect commercial comparison. A bare coil in bulk packaging and individually protected clean rods are different deliverables. Ask each bidder to say whether cleaning, straightening, cut ends, protective wrapping and special spools are included.
5. Which records should travel with each lot?
The material test certificate should identify the heat or lot and the specification and grade actually supplied. Filler-wire documentation should identify its classification and lot as required by the purchase order. When a coil is repacked or cut into lengths, its identity must remain traceable to the parent lot.
| Evidence | What it answers | Scope to agree |
|---|---|---|
| Material or filler certificate | What grade/classification and tests belong to this heat or lot? | Document type, standard edition and lot link. |
| Dimensional report | Does the supplied size meet the ordered tolerance? | Sampling frequency and measurement points. |
| Surface or cleanliness record | Has a special surface requirement been checked? | Method, acceptance limit and responsible party. |
| Pack list and labels | Can each spool or bundle be received and traced? | Spool/bundle ID, net length or mass and lot marking. |
Do not pay for a report that cannot support your release decision. A generic certificate accompanying a mixed shipment is weak evidence if it cannot be connected to the specific spool or bundle received. Conversely, if ordinary material wire only needs heat-level identity, requiring a full set of special-process reports may add cost without resolving a real risk.
What should happen at incoming inspection?
Receiving staff need a practical way to check the order without unspooling and damaging it. That usually means an external spool or bundle label with the material identity, lot, size and quantity, backed by a pack list and certificate. The buyer can then check package damage, count, label-to-certificate consistency and a defined sample of dimensions or surface condition. If the customer requires inspection along the whole wire length, that is a much more demanding agreement; the method and reporting scope should be discussed before quotation.
Record nonconformities against the delivered package ID rather than only the shipment number. That makes it possible to quarantine one spool while preserving the status of the others. A sound traceability plan is a time saver when a later forming or feed problem appears: it lets buyer and supplier determine whether the issue is confined to a package, a lot or the application setup.
6. Why do titanium-wire quotations vary?
The metal grade and source matter, but so do reduction steps, condition, yield, surface preparation, straightening and packaging. Very fine wire or tight diameter variation can require more process control and produce less usable output. A small trial order may carry setup and minimum-process charges that disappear—or change form—at higher volume. None of those effects is captured by comparing a single price per kilogram.
Ask suppliers to show the quoted form, net length or mass, package, material standard, included tests and any assumptions. If you expect recurring demand, describe the likely annual volume separately from the first release. That allows a useful discussion of repeatability and supply planning without pretending that a one-off sample price is the production price.
Useful comparison: compare cost per usable length or accepted spool for a feed process, or per qualified filler package for welding—not only cost per mass of metal.
7. What should you send for a comparable RFQ?
- End use and whether the product is general wire, filler rod/wire or precision feedstock.
- Grade or filler classification, governing standard and edition, and required condition.
- Diameter, tolerance, required continuous length, quantity and expected repeat volume.
- Coil, spool or straight form; spool drawing, cut length and packaging limits if relevant.
- Surface/cleanliness criteria, required material and inspection records, and delivery location.
If the job involves a machine, a welding procedure or a customer-controlled drawing, attach the relevant interface information. HELE can then discuss titanium wire options against the actual use, and identify which requirements need source or process confirmation before quotation.
Questions buyers often ask
Can I use ASTM B863 wire as welding filler?
Not by designation alone. A welding application needs the specified filler classification and procedure requirements reviewed. Ask for a documented comparison and approval before any substitution.
Is the smallest advertised diameter a standard stock item?
Not necessarily. Confirm the exact grade, condition, tolerance, available continuous length, package and quantity for the requested diameter.
What is the most common missing RFQ detail?
The intended delivery form. Coil, spool and straight cut rods can require different processing, inspection and packaging even at the same diameter.